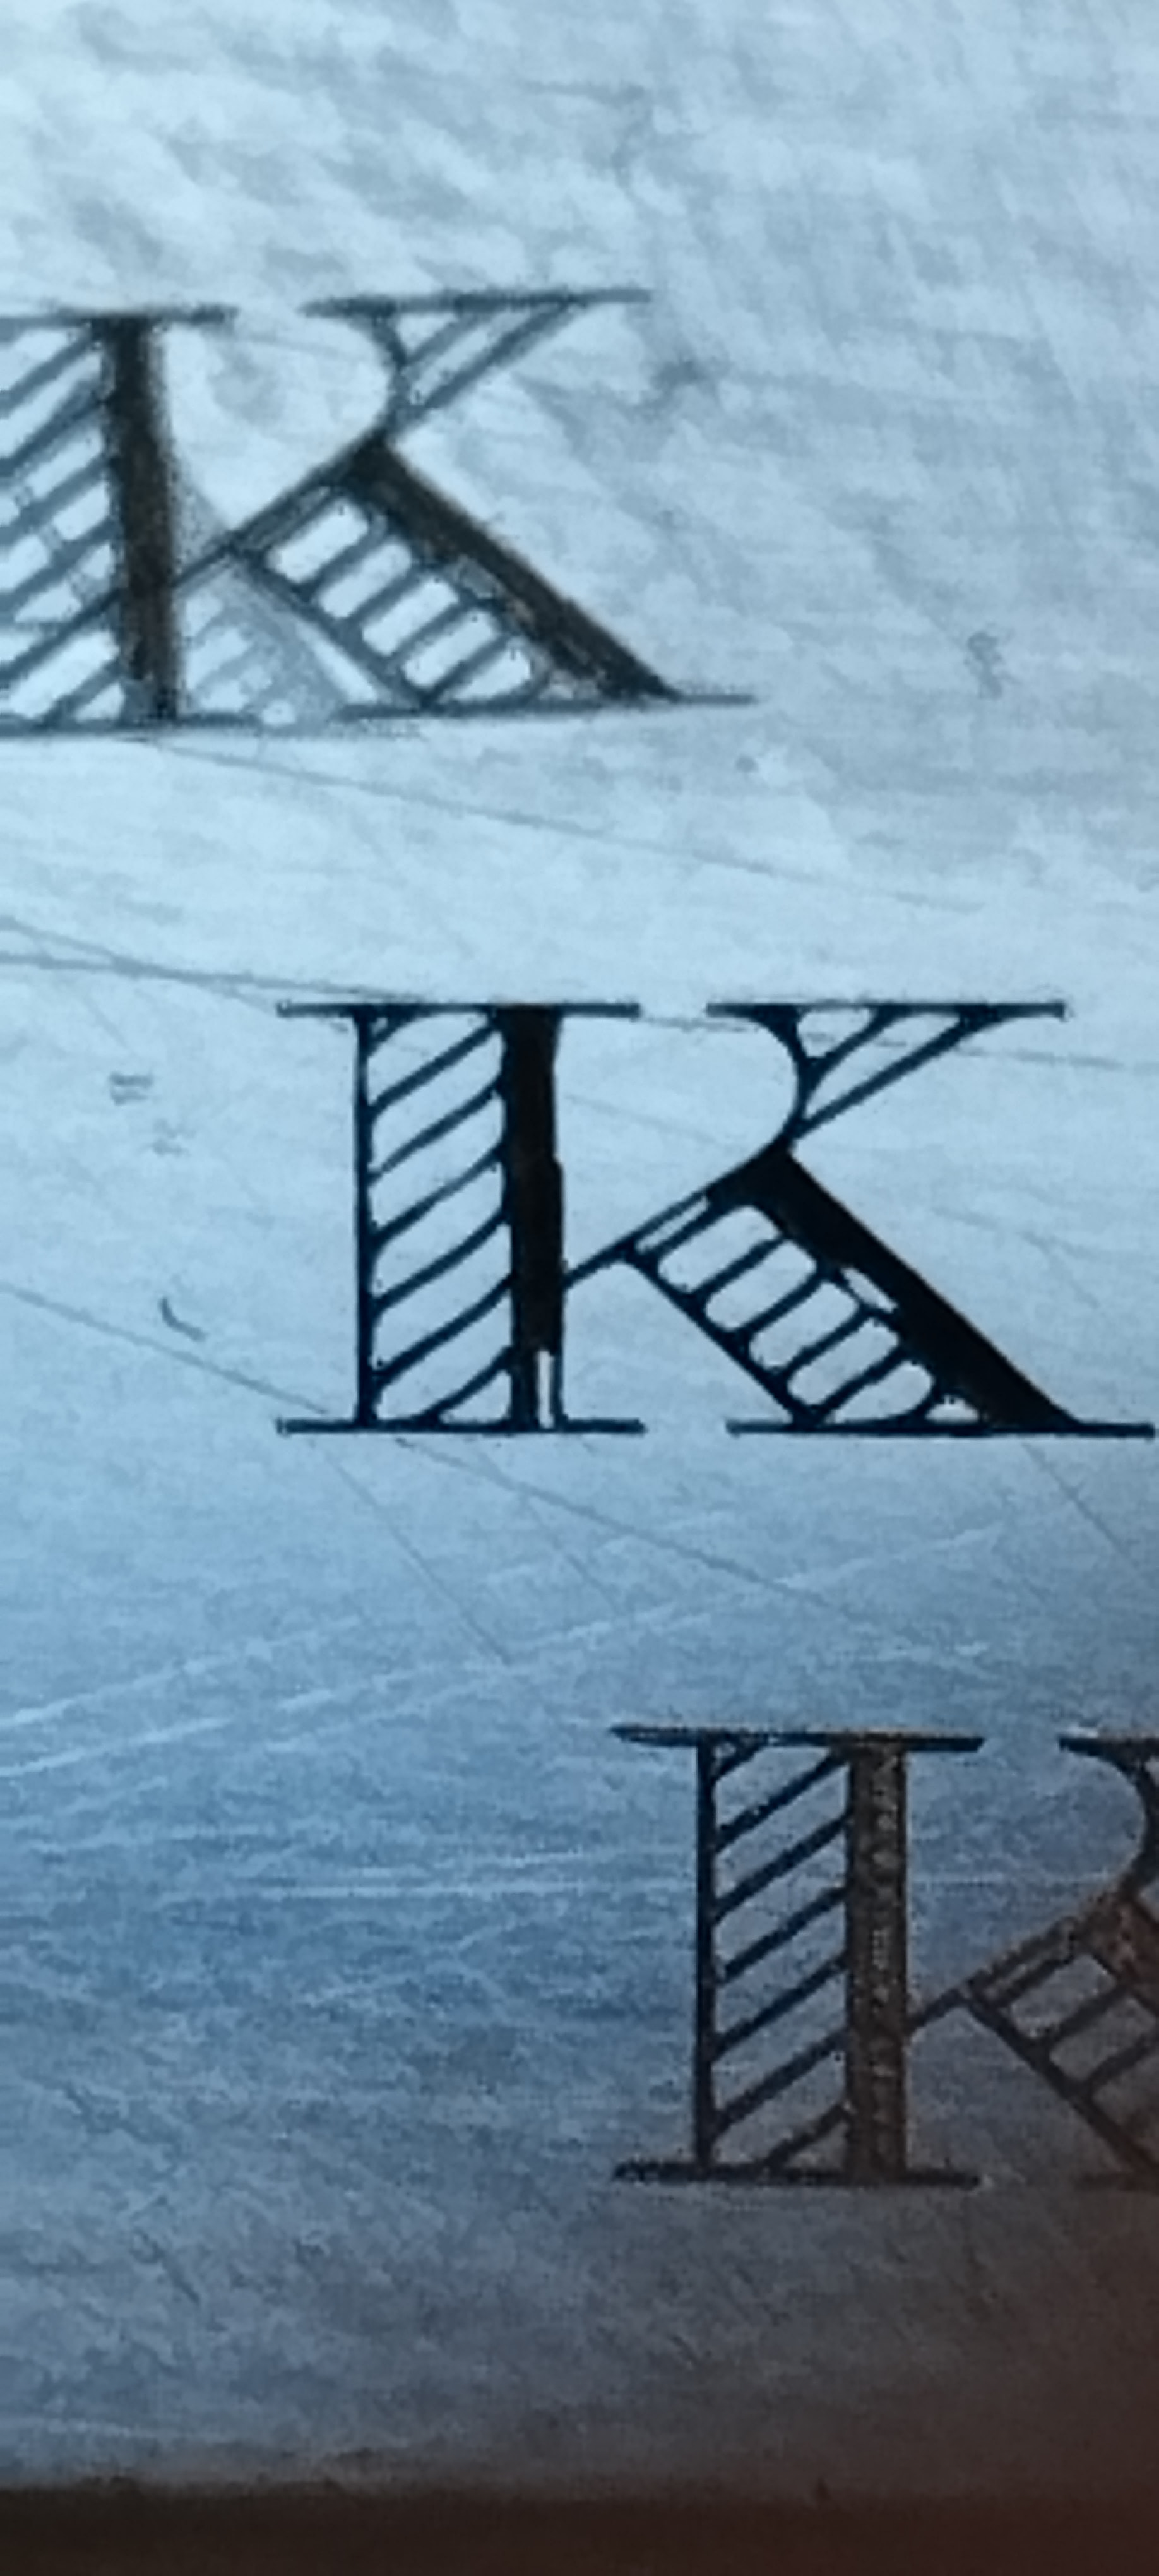I am trying to engrave mild steel to produce an ink printing plate.
As shown in the attached image, the letters are approximately 2 mm high and contain both solid areas and fine hatch lines.
My goal is to achieve an engraving depth of 0.5 mm while preserving the finest details.
What laser parameters (power, speed, frequency, pulse width, hatch spacing, fill type, number of passes, and focus strategy) would you recommend to achieve this with the best possible quality?
I have been experimenting with several parameter combinations, such as:
Fill Type: Offset Fill
Frequency: 79 kHz
Speed: 500 mm/s
Number of Passes: 120
Power: 20%
Hatch Spacing: 0.0010 mm
The results are fairly good overall. However, the solid areas are not deep enough, and the engraving is sometimes uneven. Some small areas of steel remain unengraved, as if tiny islands of material are left behind instead of being completely removed.
Do you have any recommendations for improving the engraving quality while achieving a depth of approximately 0.5 mm and preserving these very fine details?
This can be caused by impurities or the variable density of the steel. Like every other material we make or grow, perfectly even density is wishful thinking.
As you can see on the picture, parts of steel remain. It’s everytime at the same position in the letter. Wherever i try in the steel plate. I don’t think it’s a question of density so
Along with @ednisley comment about uploading the source files and image, what lens are you using?
I’m not sure what you expect as output. It has apparent shades of gray in the original image or is this an actual vector file?
I don’t think you want offset-fill operation doing this, but…?
I don’t use hatching, so I’m wondering about the hatch spacing meaning?
If this isn’t a typo, and it’s the interval, then it’s likely too small. Although we do it for special applications, it’s usually questionable doing this with a scan interval that is smaller than your spot size.
Even an F100mm lens has a spot size of about 15 microns (0.015mm), your interval is set to 0.0010mm will cause it to cover the same area 15 times. Even at 0.010mm it will scan each 1.5 times.
Do you need it engraved or do can it be marked, such as with an oxide layer?
Usually for depth, I choose 45kHz along with a slow scan speed and cleanup passes relatively often. 45kHz is where my source (60W) produces it’s most power, according to the manual.