Creating Better relief carvings MillMage Pro help Please

Hey there folks,

My name is Pat and I have a Genmitsu 6050 XL Plus at the moment. I’m still making mistakes, learning as I go, and actually enjoying the problem-solving side of things!

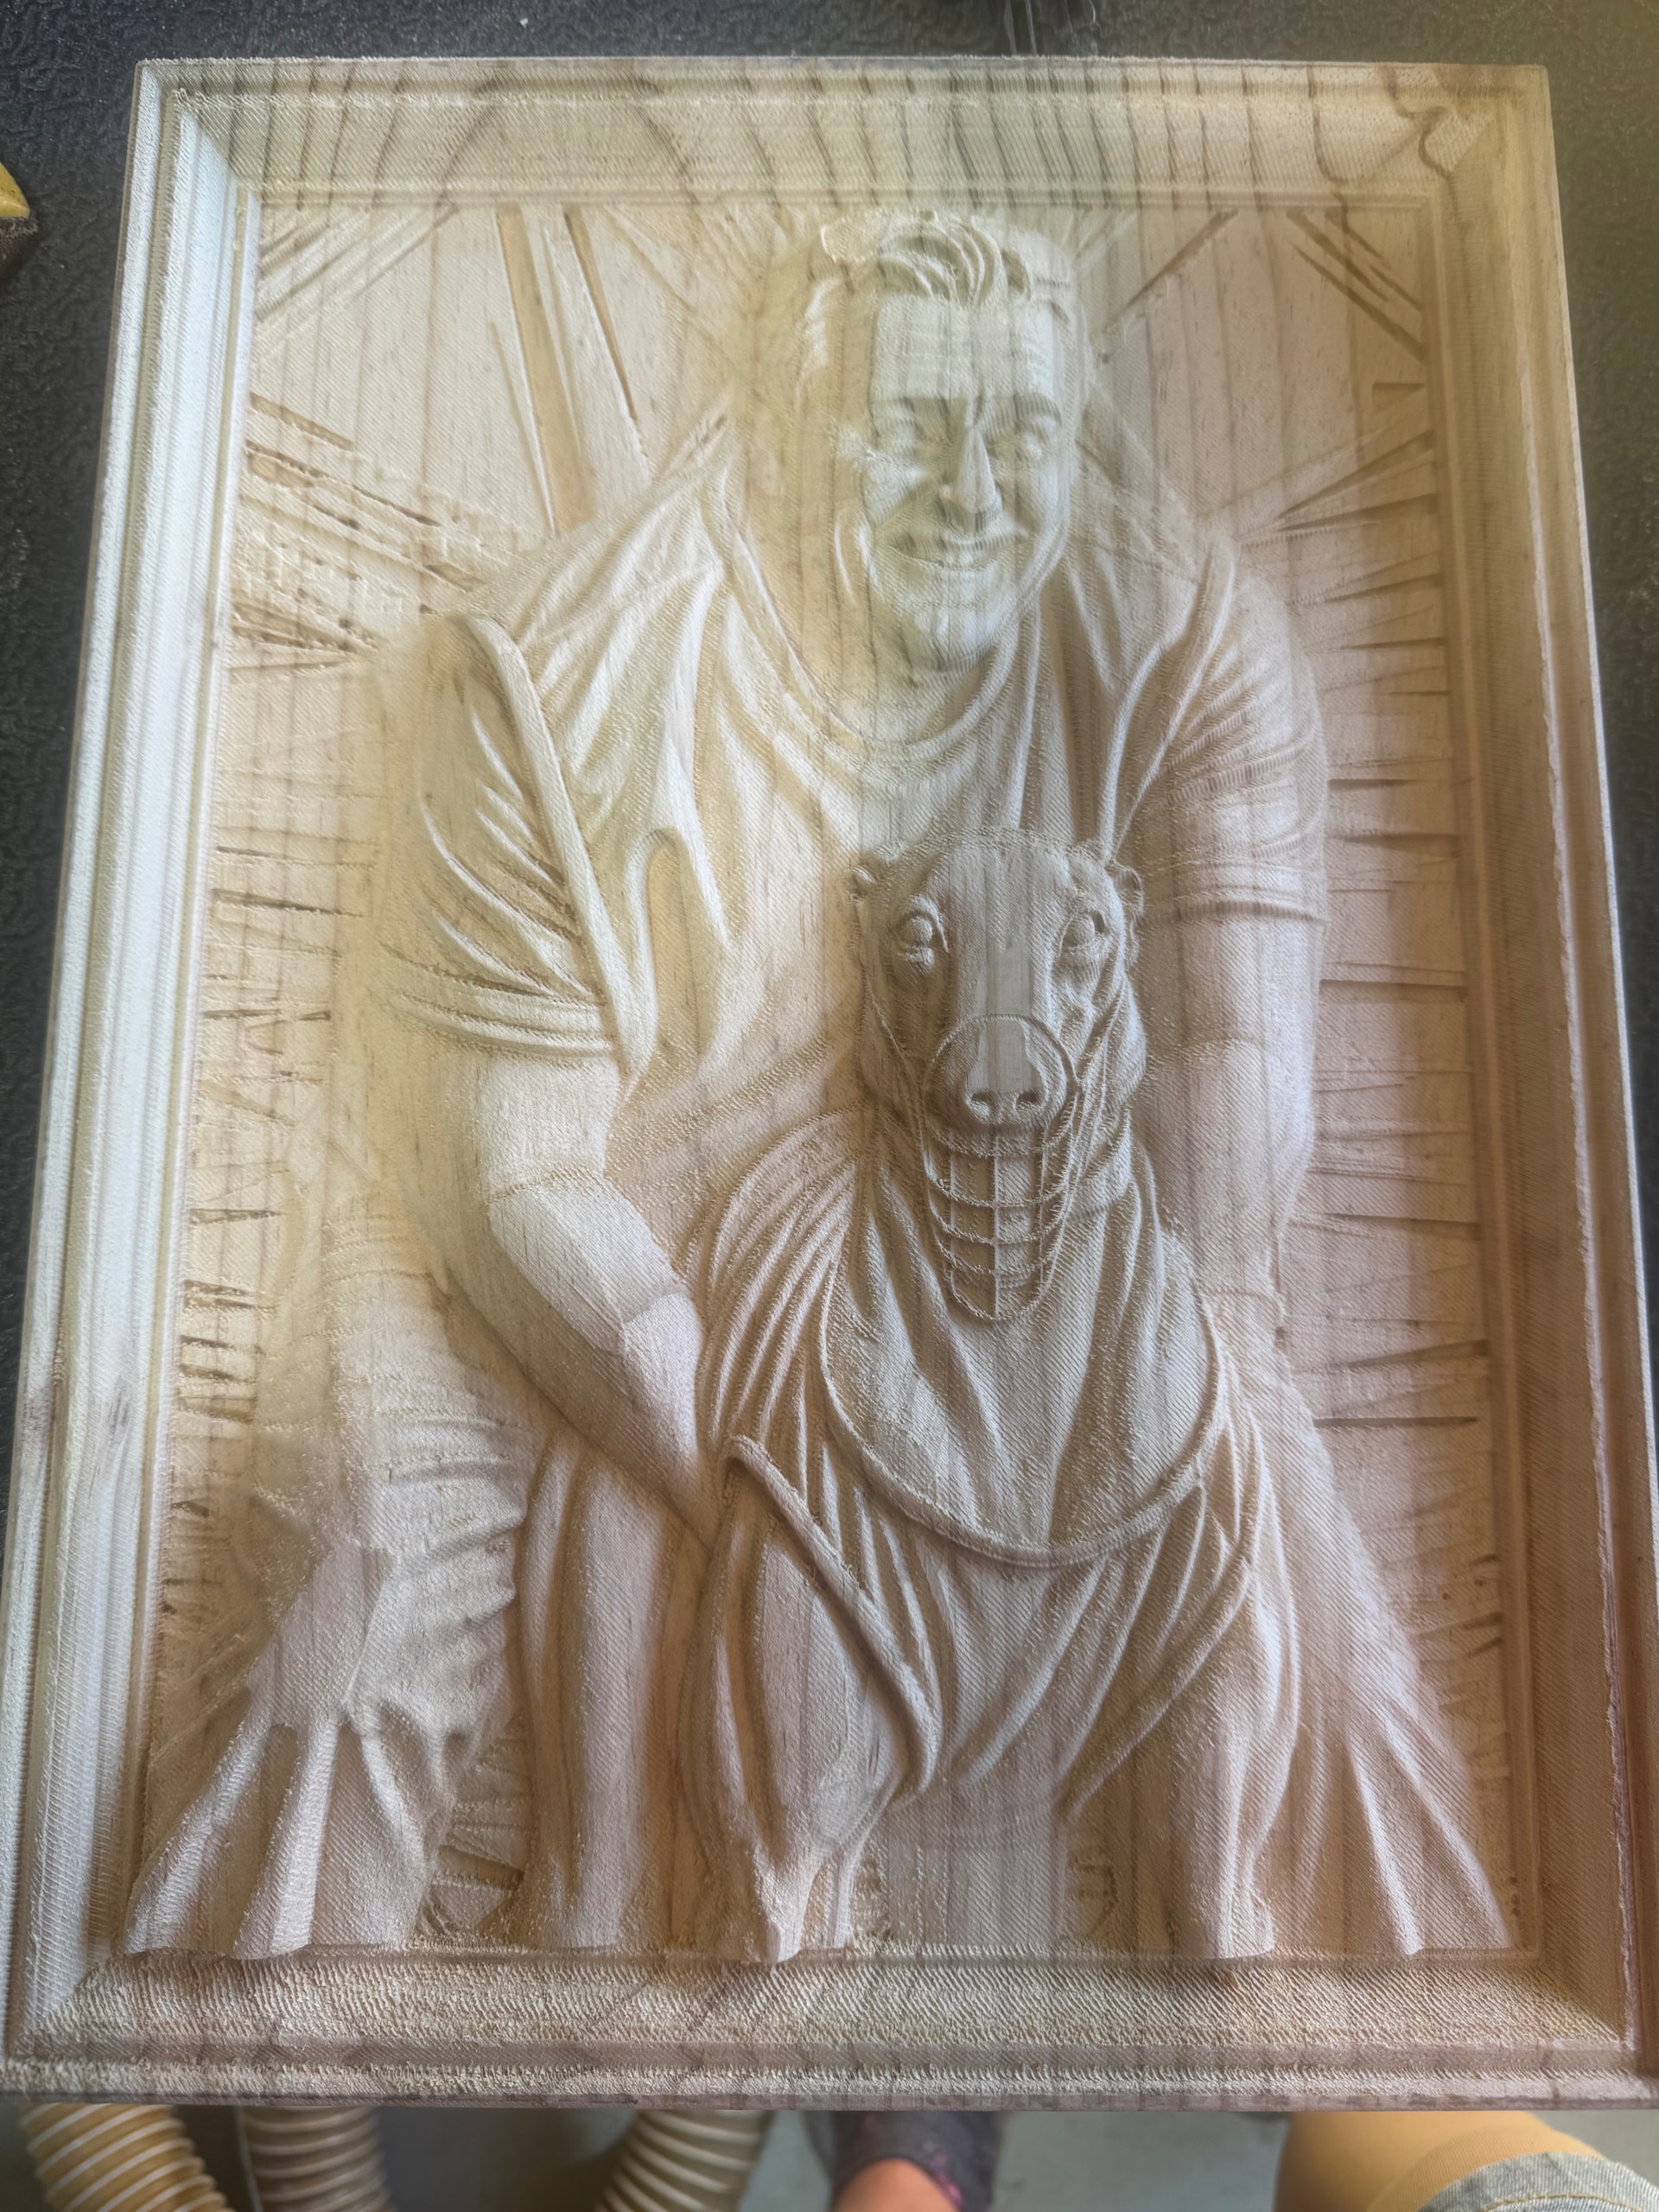
I decided to try my hand at a picture that Yohan converted to an STL file for me — I think! :grinning_face_with_smiling_eyes: Anyway, I did the carving and only used cheap pine as this was really a test.

But here’s why I’m asking for some advice from people who do this sort of relief carving regularly. It takes bloody hours to confirm you’ve stuffed it! HEHE.

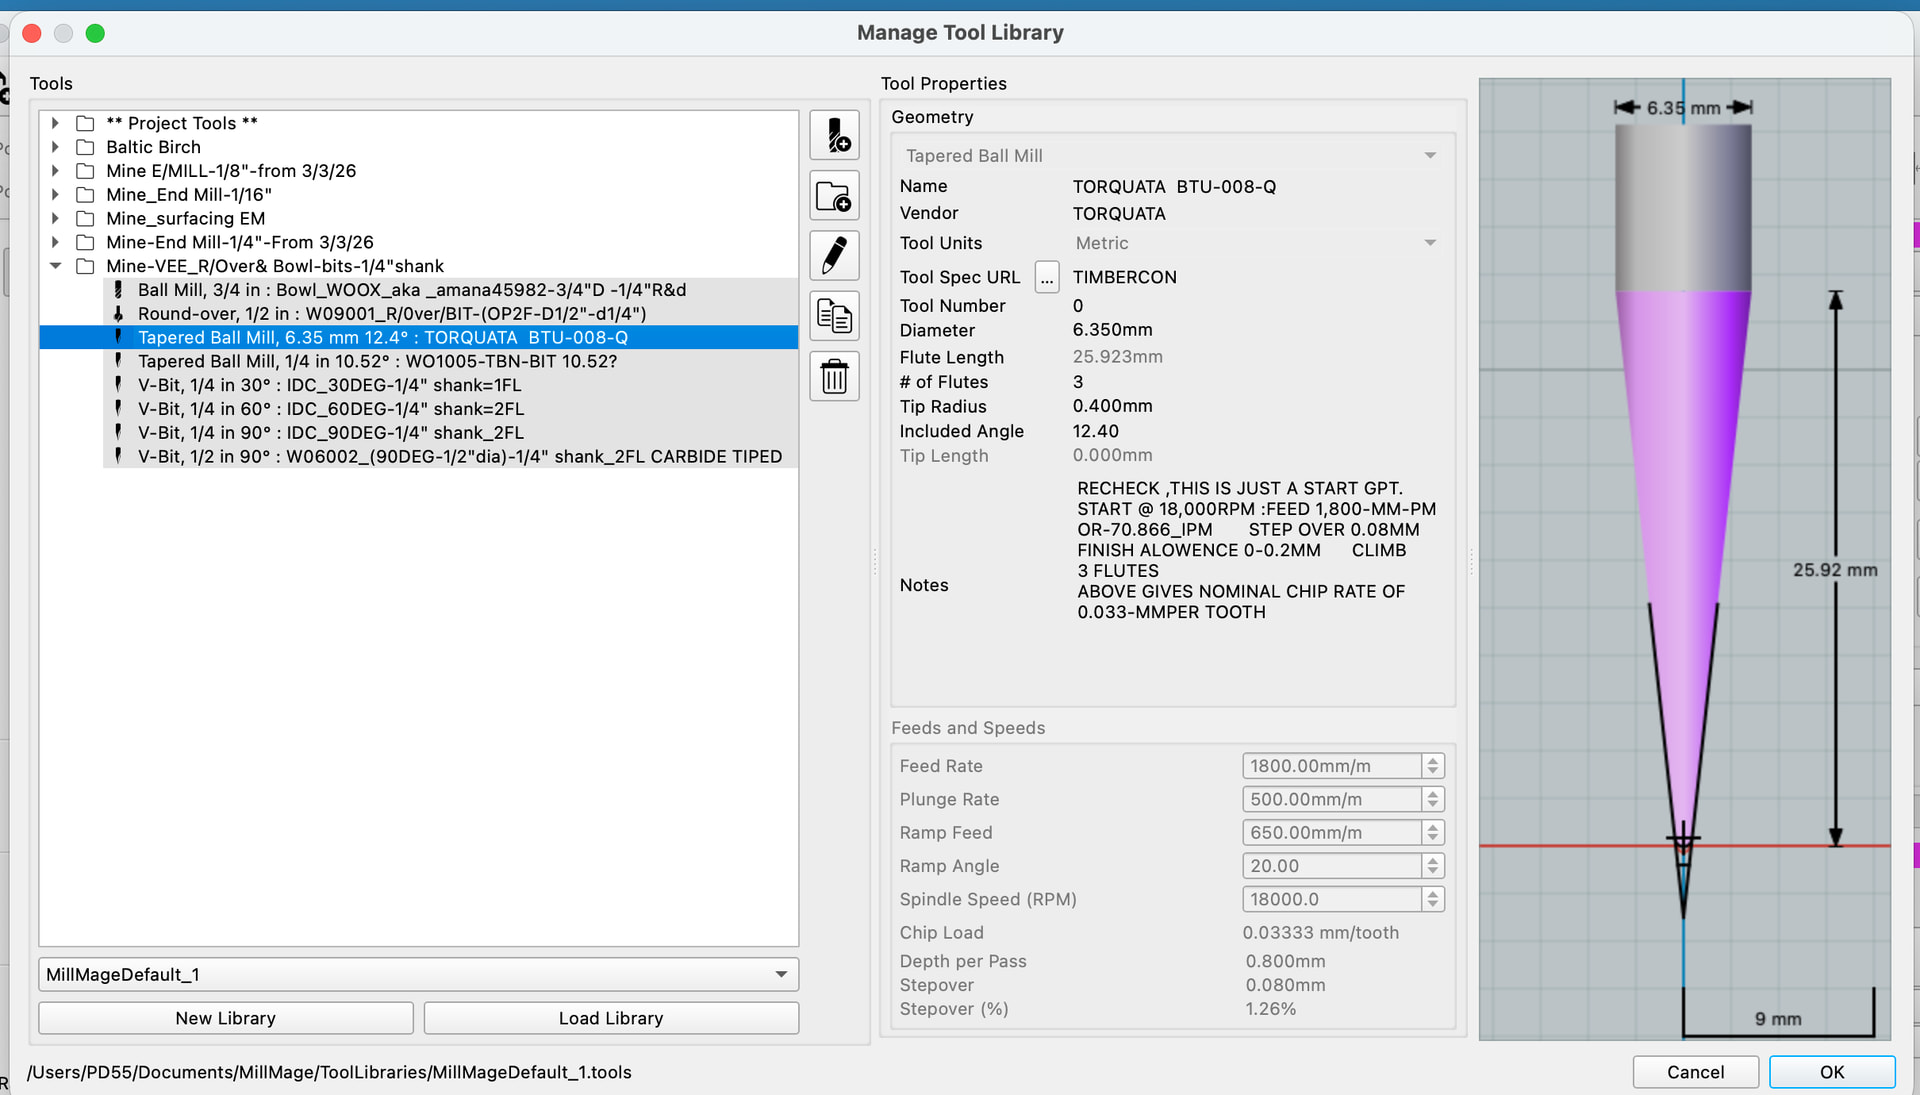
I’m using a Torquata 0.8 mm diameter tapered ball nose (TBN) bit. For the finishing operation I used a 0.384 mm stepover, all done in MillMage Pro.

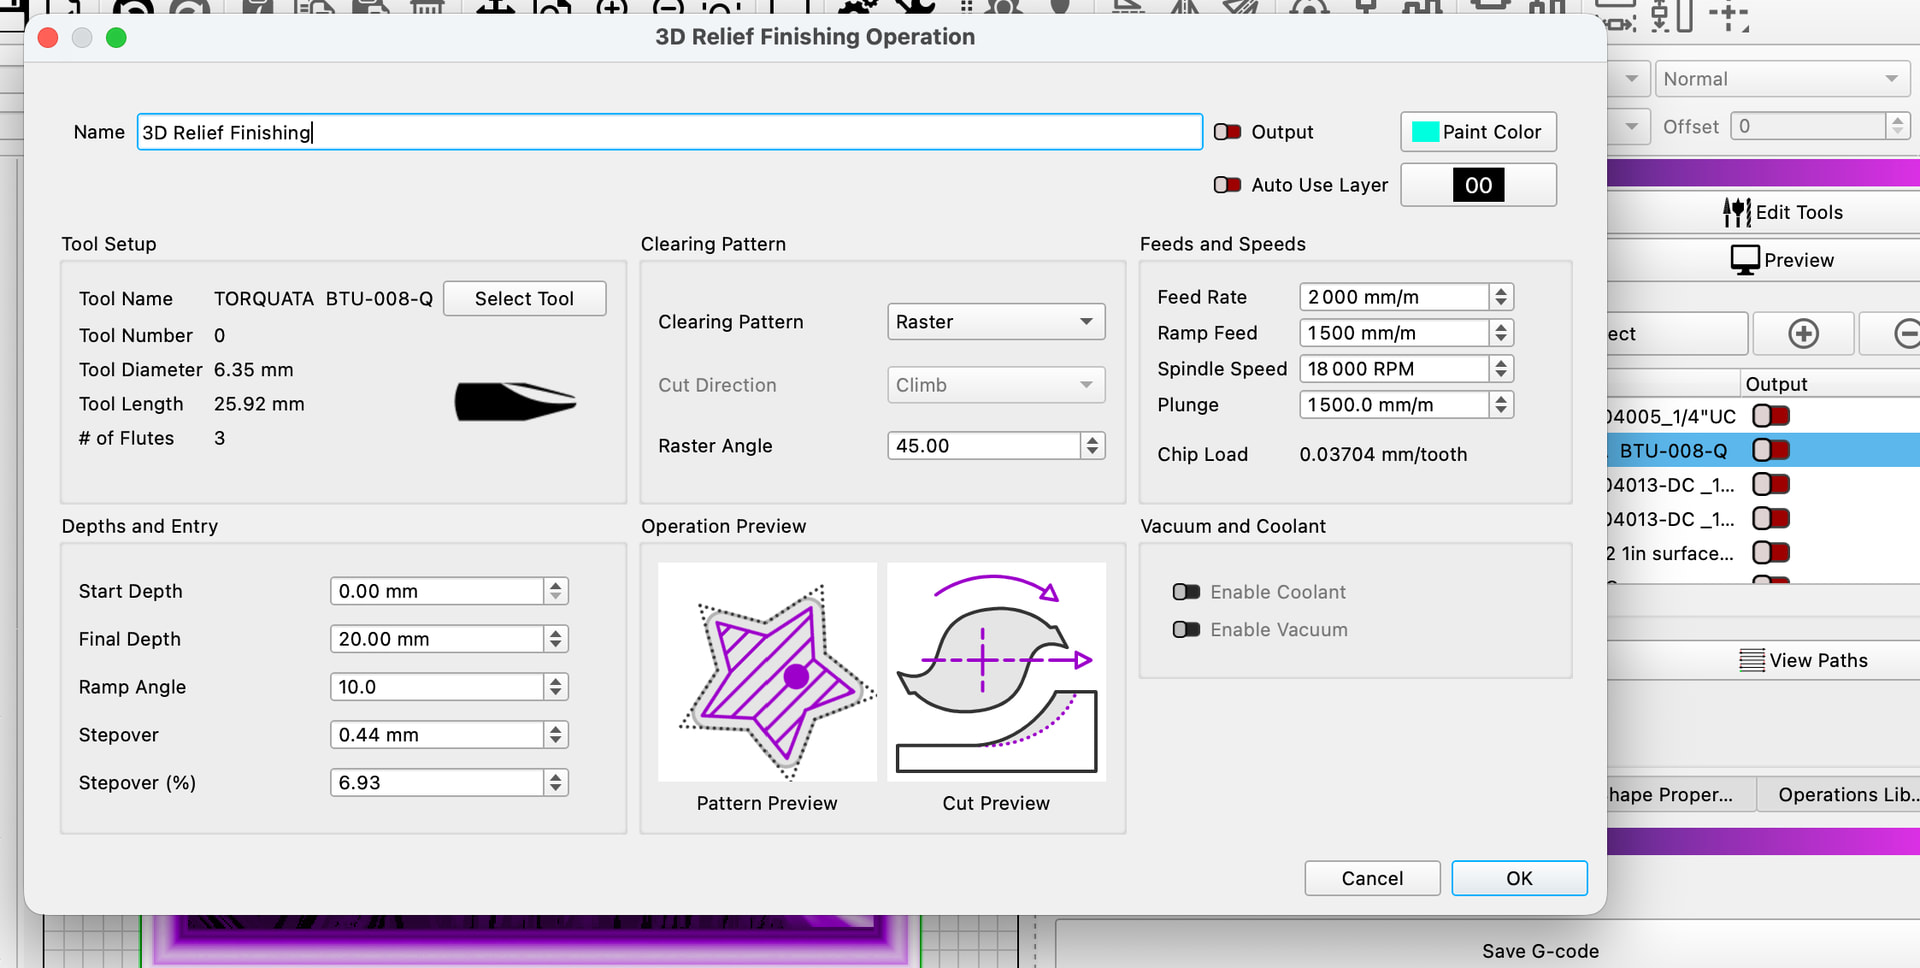
I’m going to try to add a couple of photos along with the finishing-operation settings.

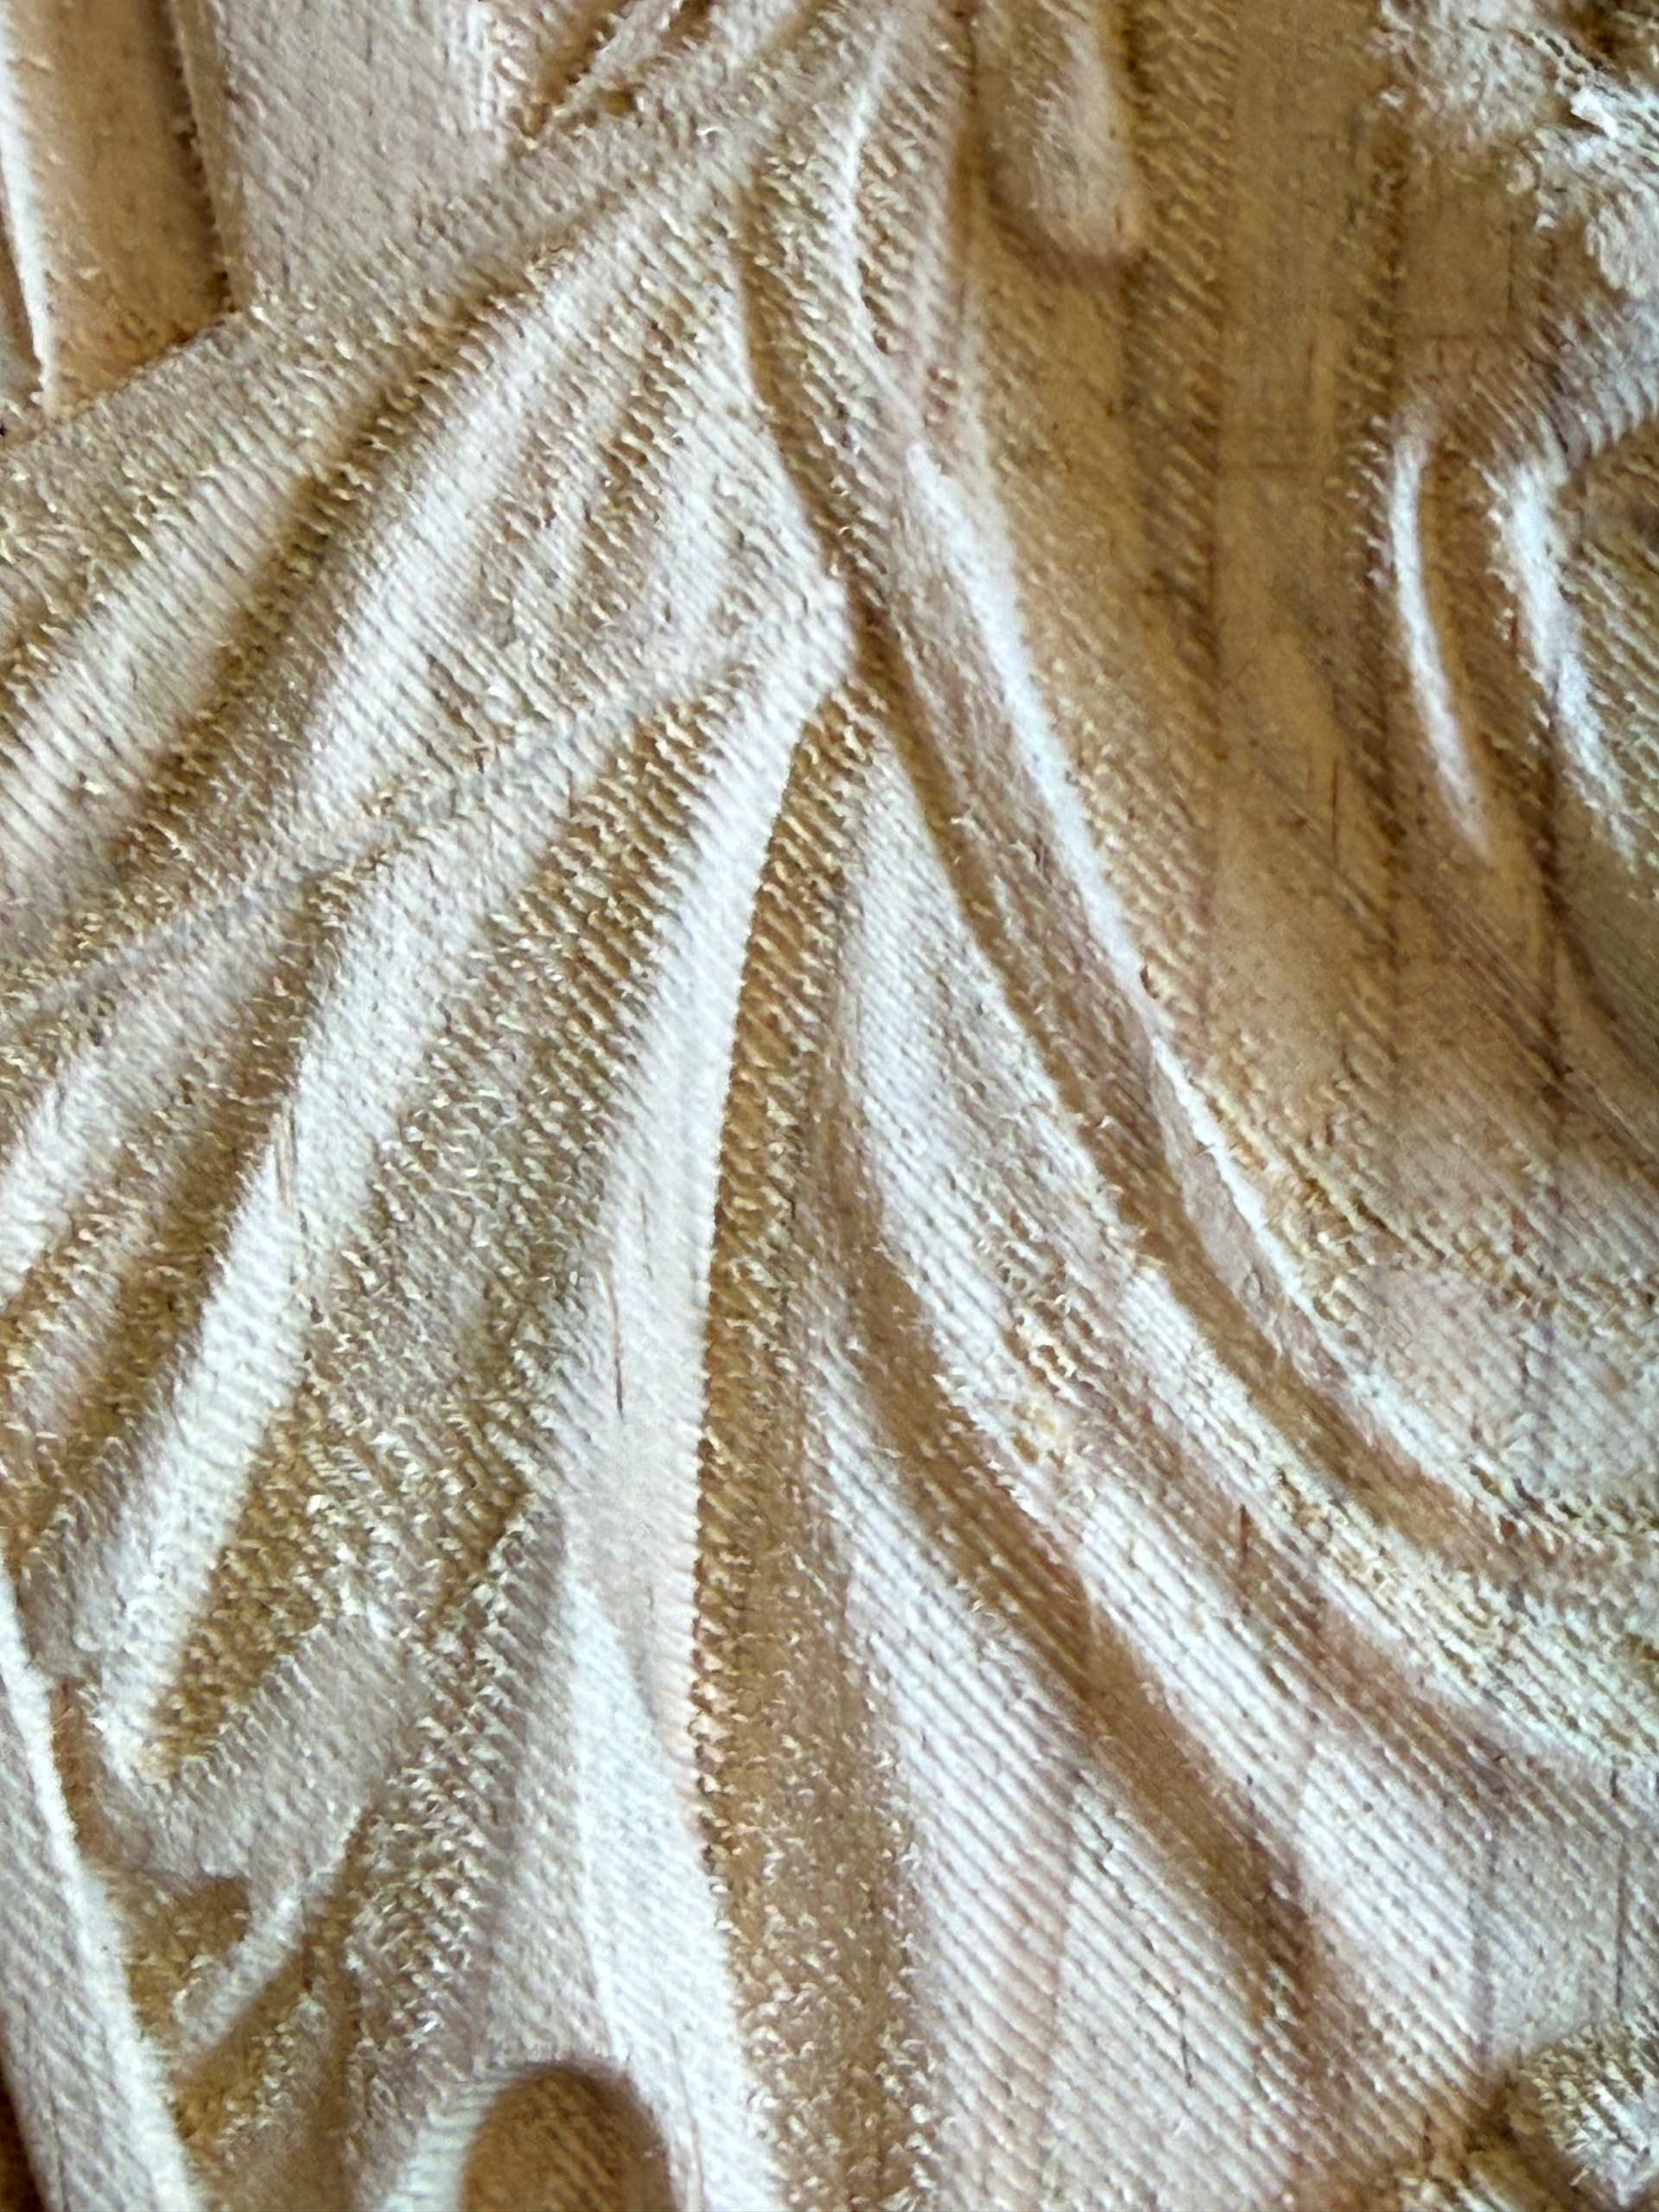
There are a LOT of visible lines in the finished carving. I thought my stepover would have been adequate, but looking at the result, maybe not?

I’m in Australia, so obviously we have different timbers available, but cheap and nasty pine is probably cheap and nasty pine worldwide! I understand it isn’t the ideal timber for this sort of work.

So, a few questions:

1. Is the pine likely to be a major part of my problem?

2. Would you suggest reducing the stepover considerably from 0.384 mm?

3. I’m running the finishing pass at 45°. Would that make much difference to the final result?

4. One suggestion was to run another finishing pass in the opposite direction (-45°), basically creating a cross-hatch pattern to clean it up.

That sounds reasonable, but it takes the machining time from around 6 hours to 11 hours. That’s a long time to wait just to discover it still isn’t right!

5. Is there a way in MillMage to isolate a small section of a relief for testing?

I tried using a mask so I could machine just a small test area, but it doesn’t appear to work with reliefs — unless I’m doing something wrong.

I don’t really want to simply shrink the entire relief because that isn’t the same test.

In hindsight, I probably should have asked Yohan if he could cut out a small section of the original relief for me.

Ideally, I’d like to take something like a 100 mm × 100 mm section from a COPY of the relief and use that for testing. Then I could experiment with different woods, stepovers, angles and finishing strategies without waiting 6–11 hours every time.

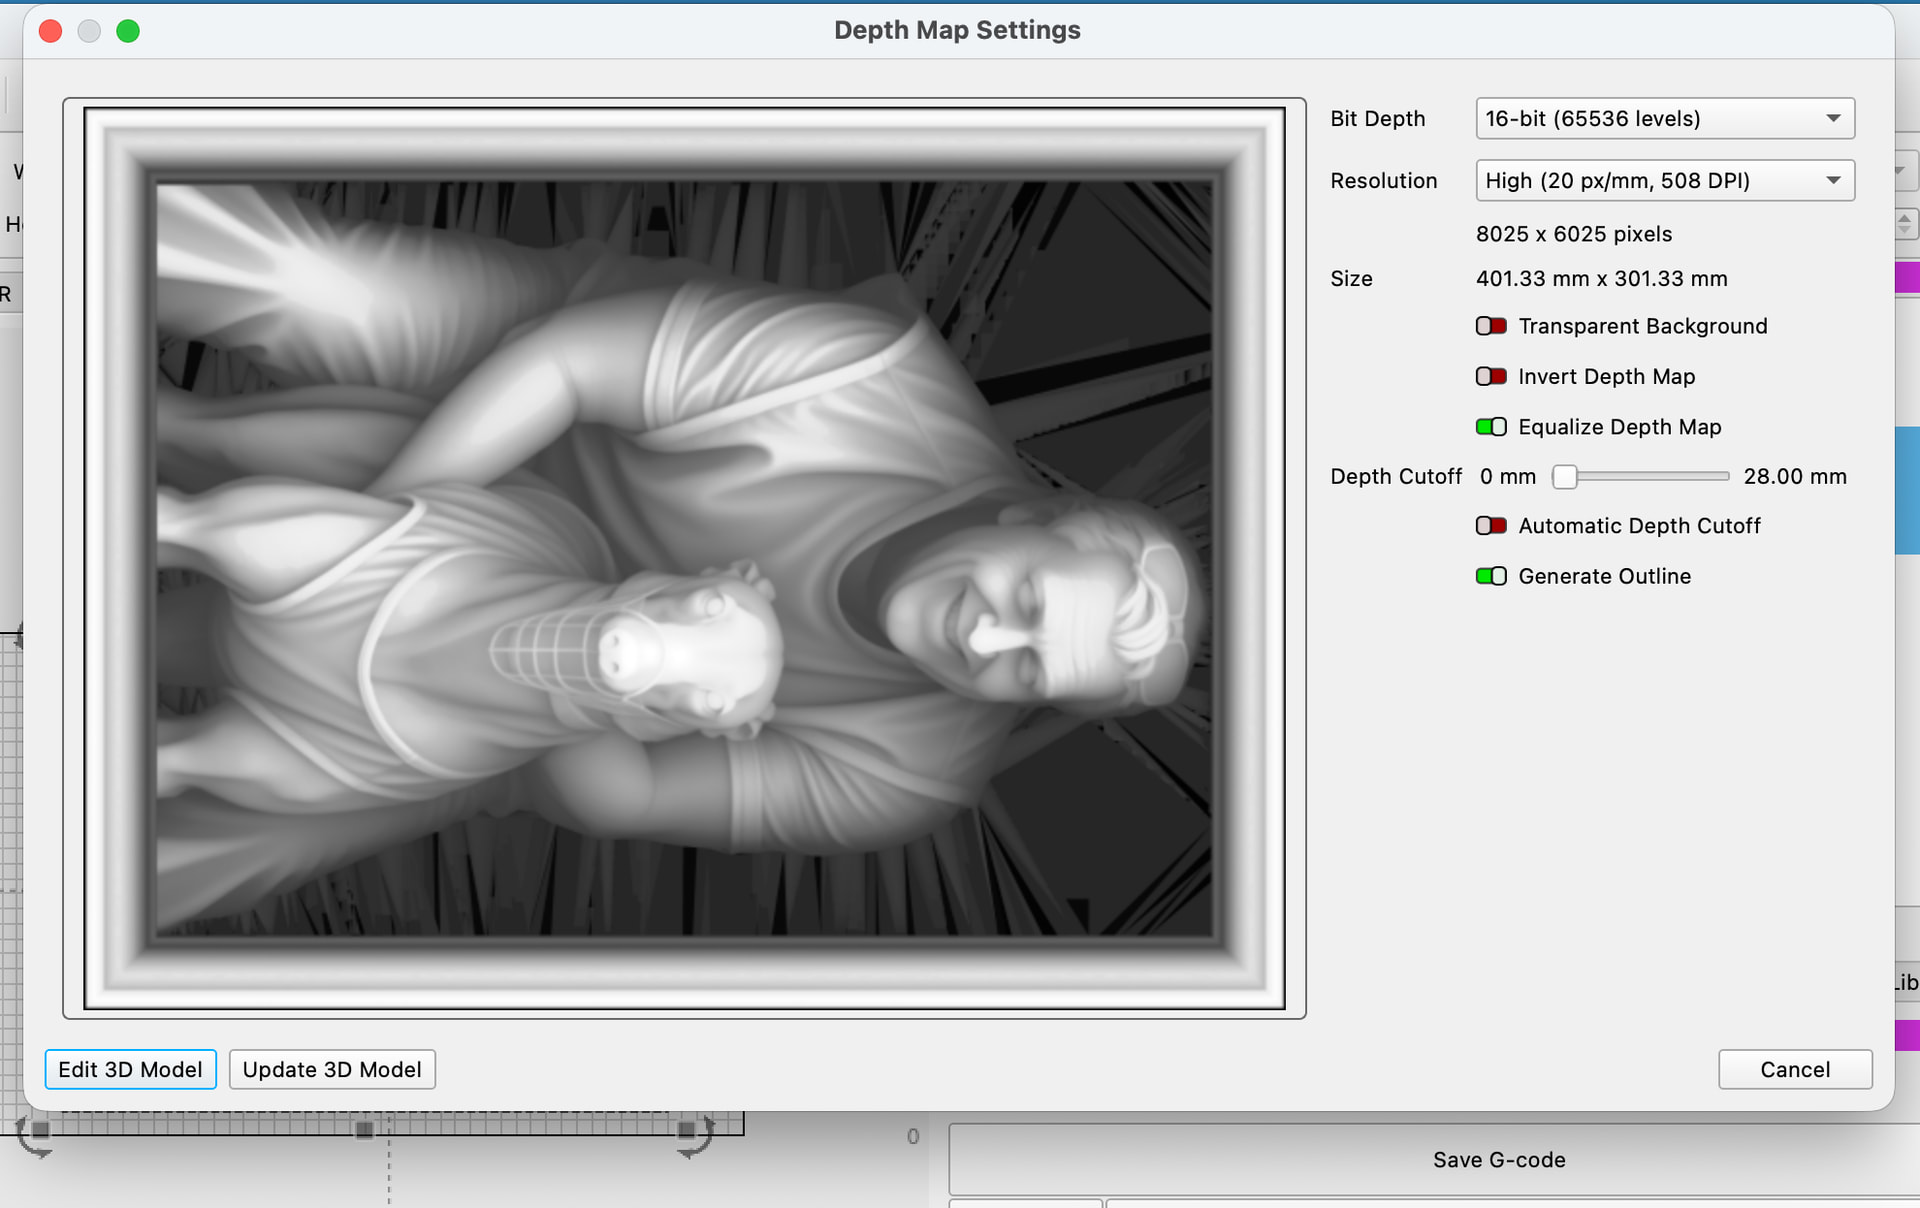
For this particular job I also used the option that changes the background so the subject stands out more. I’ll experiment with that setting as well.

Any constructive advice from people doing relief carving would be greatly appreciated — particularly regarding wood choice, stepover, finishing angle and how to create a small test section of a relief in MillMage.

Thanks,

Pat

in your bit notes, it says to use a .08mm stepover. But you are using a .44mm stepover

Unrelated to the topic you are asking about. I would be interested in seeing your roughing bit settings.

It appears you are using a 48% stepover. I think something like 12% or less is recommended.

Somebody in another Topic did the same, with the same result. One Reply said to make a circle poart of the operation and that would do it. I have no details on that suggestion.

Nature of the process. Adding in a Z motion for every X and Y means you multiply the time by those Z moves.

One option is to use machining foam to test with. That permits you to run at full speed.

If you got a 3D carve, even though the finish is rough, you are doing good.

pine is to soft so u will get those marks redwood does the same , i use nz totara soft but dense

, get urself some of the red scourer pads its about 320 grit , and rub it most will disappear, the other trick little brass wire brush in a dermal gets rid of the bits ur fingers wont go
i run on angle with softwood dosent seem to rip it as much

from my experience only way to minimize lines is slow right down , if u stand back 2-3 feet u cant see the lines

thanks Terry , just going through all the thoughts now mmmm must admit never herd of that wood but ill check out the availability here in Australia

the genmitsu was running flat out ! that just happens tp be 2000mm or 78IPM

thank Miky seemed to have come to the same conclusion with the preview that is nearly doubled the time , oh well miss what it is I guess …all a learning curb thanks again

thanks Jack here’s a pick of what I used was a 1/4"UC

I was useing 5.94% step over .Mikey

that’s , as I see it around 5-6% from memory was something like 5.94 ??? I put 6 in and it changed to this no so say 6 % of a diameter tip of 0.8 ??? don’t know where your getting 48% from mate???

I did not say anything about 48%. I did say .44mm if that is what you are talking about. But that is what your settings page says

Oh I see, you were talking to Mikey.

Now that I have looked at this again, it takes me a bit to study this as I still use imperial units. But first the bit. That is a very small bit. So a carve is going to take way too long. For anything over a 5 inch carve, I use the IDC Fine bit.

  • Overall length: 2.2 in
  • Flute Length: 0.75 in
  • Number of flutes: 2
  • Shank Diameter: 0.25 in
  • Cut Diameter: 0.25 in
  • Tip Radius: 0.045 in
  • Taper Angle: 10

For anything that has super fine detail in the STL or the carve is very small, I use the IDC Ultra fine bit.

  • Overall length: 2.2 in
  • Flute Length: 0.75 in
  • Number of flutes: 2
  • Shank Diameter: 0.25 in
  • Cut Diameter: 0.25 in
  • Tip Radius: 0.015 in
  • Taper Angle: 10

That will take a 10 hour carve and turn it into a 3 hour carve. A smaller bit will give you mare detail but you will reach a point of diminishing return. Where the model does not have enough resolution to take advantage of the smaller bits. Just takes longer for no reason. Cuz all the extra passes that the bit travels. And Pine is not the best to carve in. That is where all the fuzzy is coming from. But that is not where the lines are coming from.

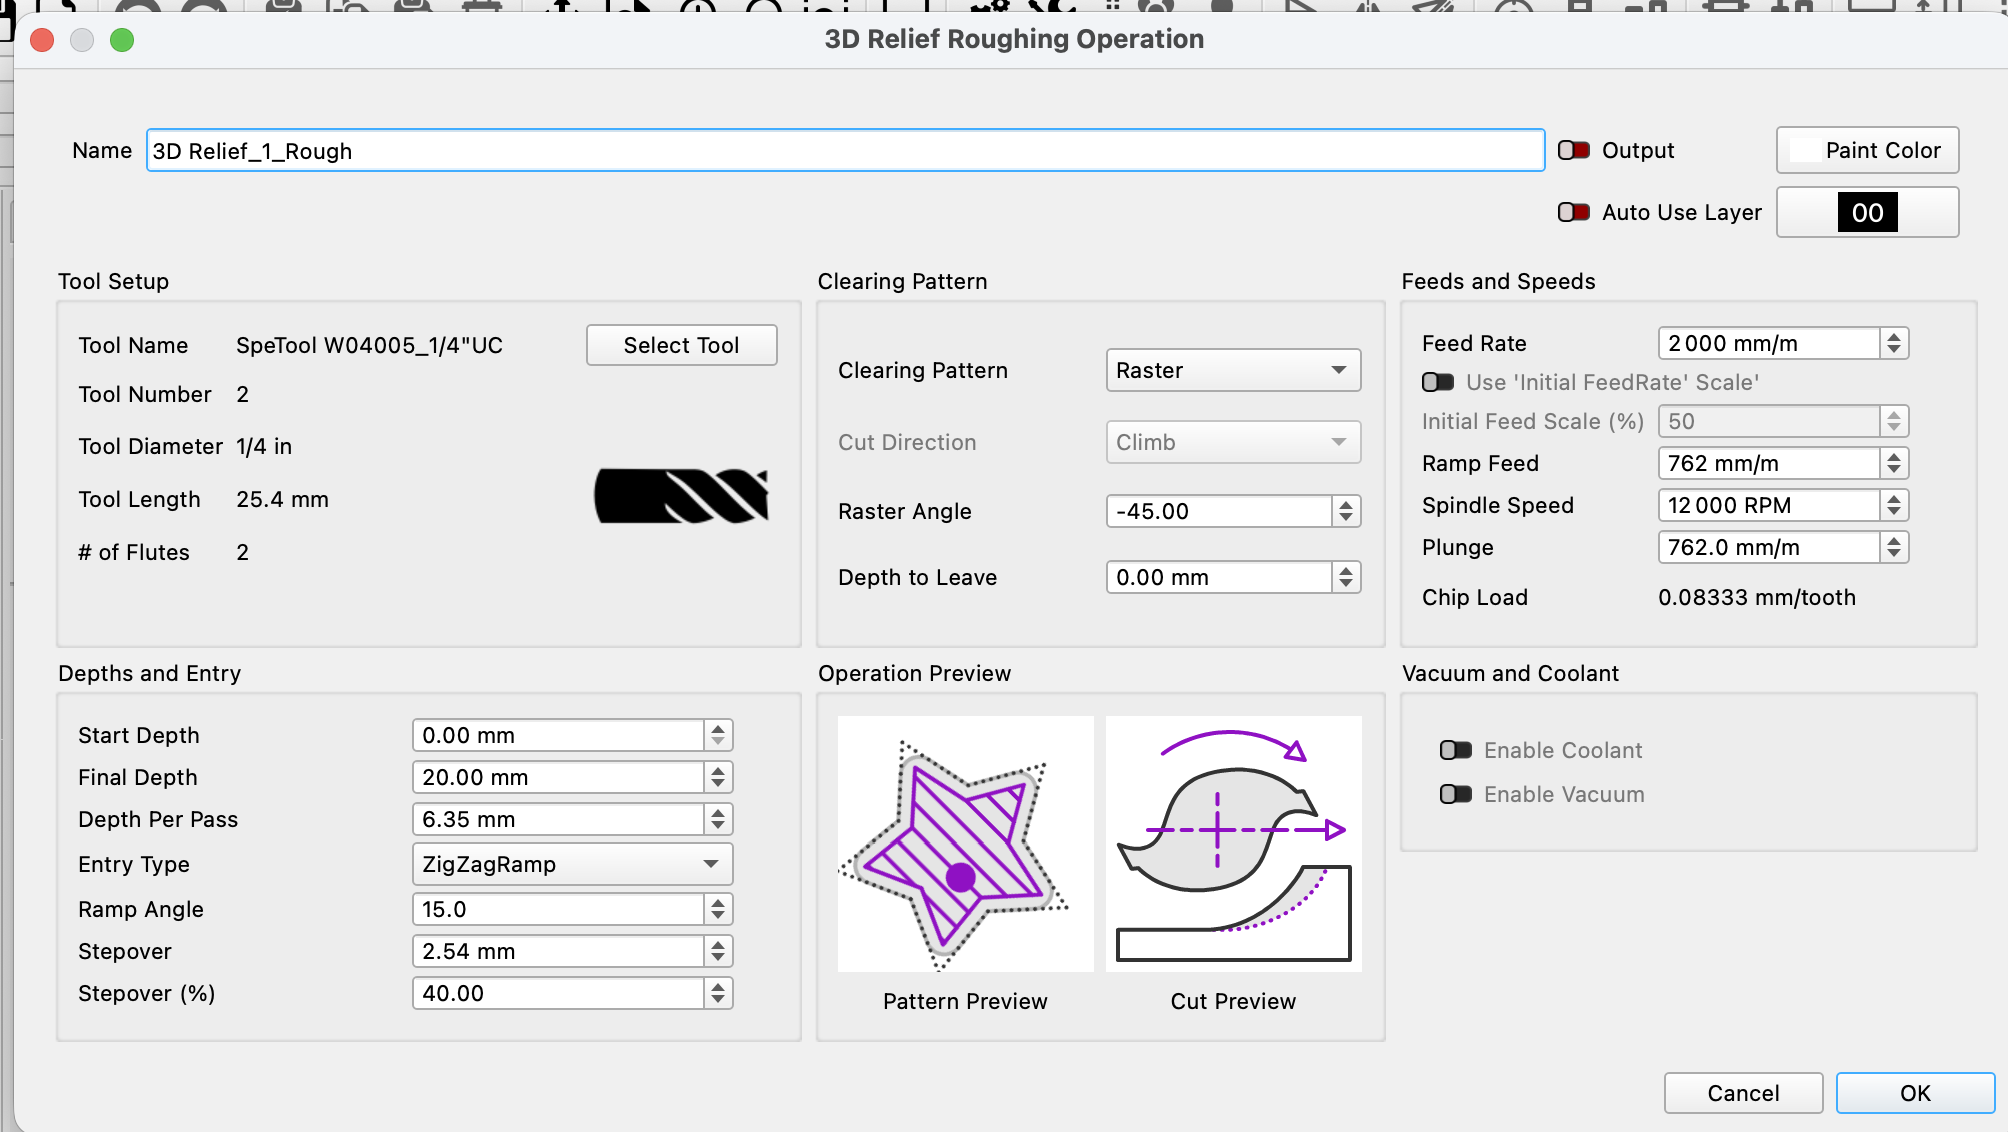
The reason I wanted to see the roughing pass settings is I think I spot some flats in your carve. around the knee and the dogs nose and the mans arm. I am seeing them in some of mine if I don’t run the roughing at full depth. If I set my roughing pass to .25 or .125 inch per pass, I get flat spots. If I run the roughing at the full final depth, the carve has no flats.This should not be happening.

I was using this with the 0.44mm stepover. Your stepover is nearly half the ball diameter.

Are you thinking Tool Diameter is the same as the Tip Diameter?

its a NZ native timber so you wont find it in oz , try searching oz wood similar to nz totara and ssee what u come up with , ive been told macracopa is prob another good one to try

To do a smaller test region, just draw a shape around the area you want to run and add it to the operation. 3D Relief and Roughing operations allow you to add shapes that define the boundary of the operation.