it’s a common mode on industrial machines. It only runs 1 line of G-Code whenever you press the Go Button (whatever form that takes on you machine). it’s really helpful when you’re setting up new programs to prove them.
Option Stops [M01]
are related, but they’re usually at the end of each operation (this is usually done by your post and as preference, but it’s a G-Code command) and are skipped by default. but if you enable Option Stop Mode, the machine stops/pauses at those commands.
eg.: M00 pauses regardless, for things like a tool change or clearing chips or whatever. things that need to be stopped for during every run.
M01 Pauses only if Option Stop Mode is enabled. so if you put it at the end of each operation, when you run the Program for the first time, you can verify that each Op is doing what it’s supposed to, but when the program is proven, you can just turn off Option Stop mode and run the program.
do either of these exist in Millmage, perhaps by a different name? i haven’t been able to find them.
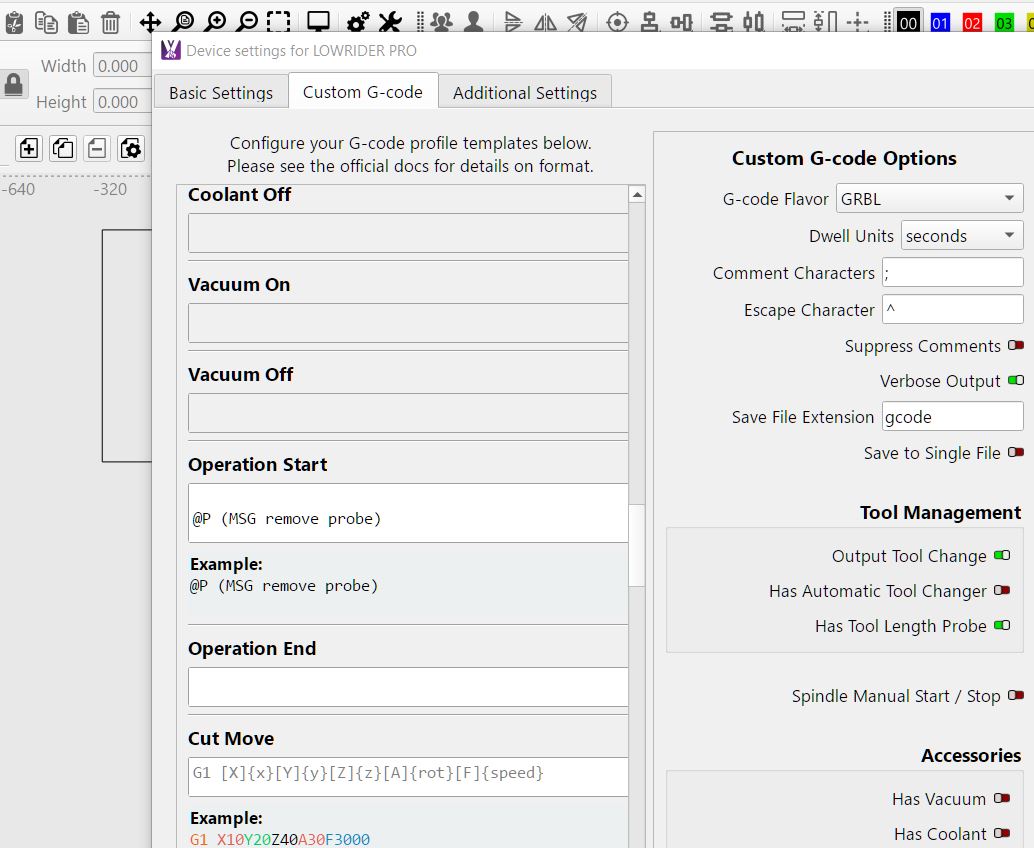
Not a “switch” that I know about, but did you try adding M1 to the end of the Cut Move and Rapid Move code in the Custom GCode section?
Altough not as easy as a switch, but not difficult to add and remove as needed.
Curious, have you actually edited the GCode file to confirn the M1 command behaves as you expected? Manufacturers do strange thing with the source code they compile for their controllers.
My solution is to run the program without a tool in the spindle. No unpleasant surprises that way.
hopefully on right track with what ur asking , @P is MM M00 ,M01 dont recall that on the list there is a list in docs of usable codes, dont ask me which section i cant remember
now my machine pauses after its tool probe , which gives me time to add dust shoe etc , re clearing chips i just hit pause button in job control tab mid job, only down side is Z stays where you pause it you cant lift it up, , you could try adding codes to the user start and end script boxes
that would be a dry-run. good practice, but different. when doing a program with a lot of Ops, it’s a good idea to make sure to run one Op at a time, with the tool, the first time you run it. then you can check the state of the work, measure things if needed, surface finish, etc. if a tool behaves weird in one op in contact with the work, you can asses why and figure out the easiest way to fix it, like altering the Op or tool. maybe it’s speeds and feeds are too off for one opp.
Yes, I know the difference. I think Candle (GCode sender) does have the single step capability.
My “solution” was an option, not a solution. I understand that scarry first contact with the material very well. No matter what the feeds & speeds chart shows, it still makes me nervous.
Question answered in feature suggestions. No, MM doesn’t have either, yet. Single Block is planned, and they will look into Option Stop, which they described as “probably trivial.” which is great news.
 I understand that scarry first contact with the material very well. No matter what the feeds & speeds chart shows, it still makes me nervous.


