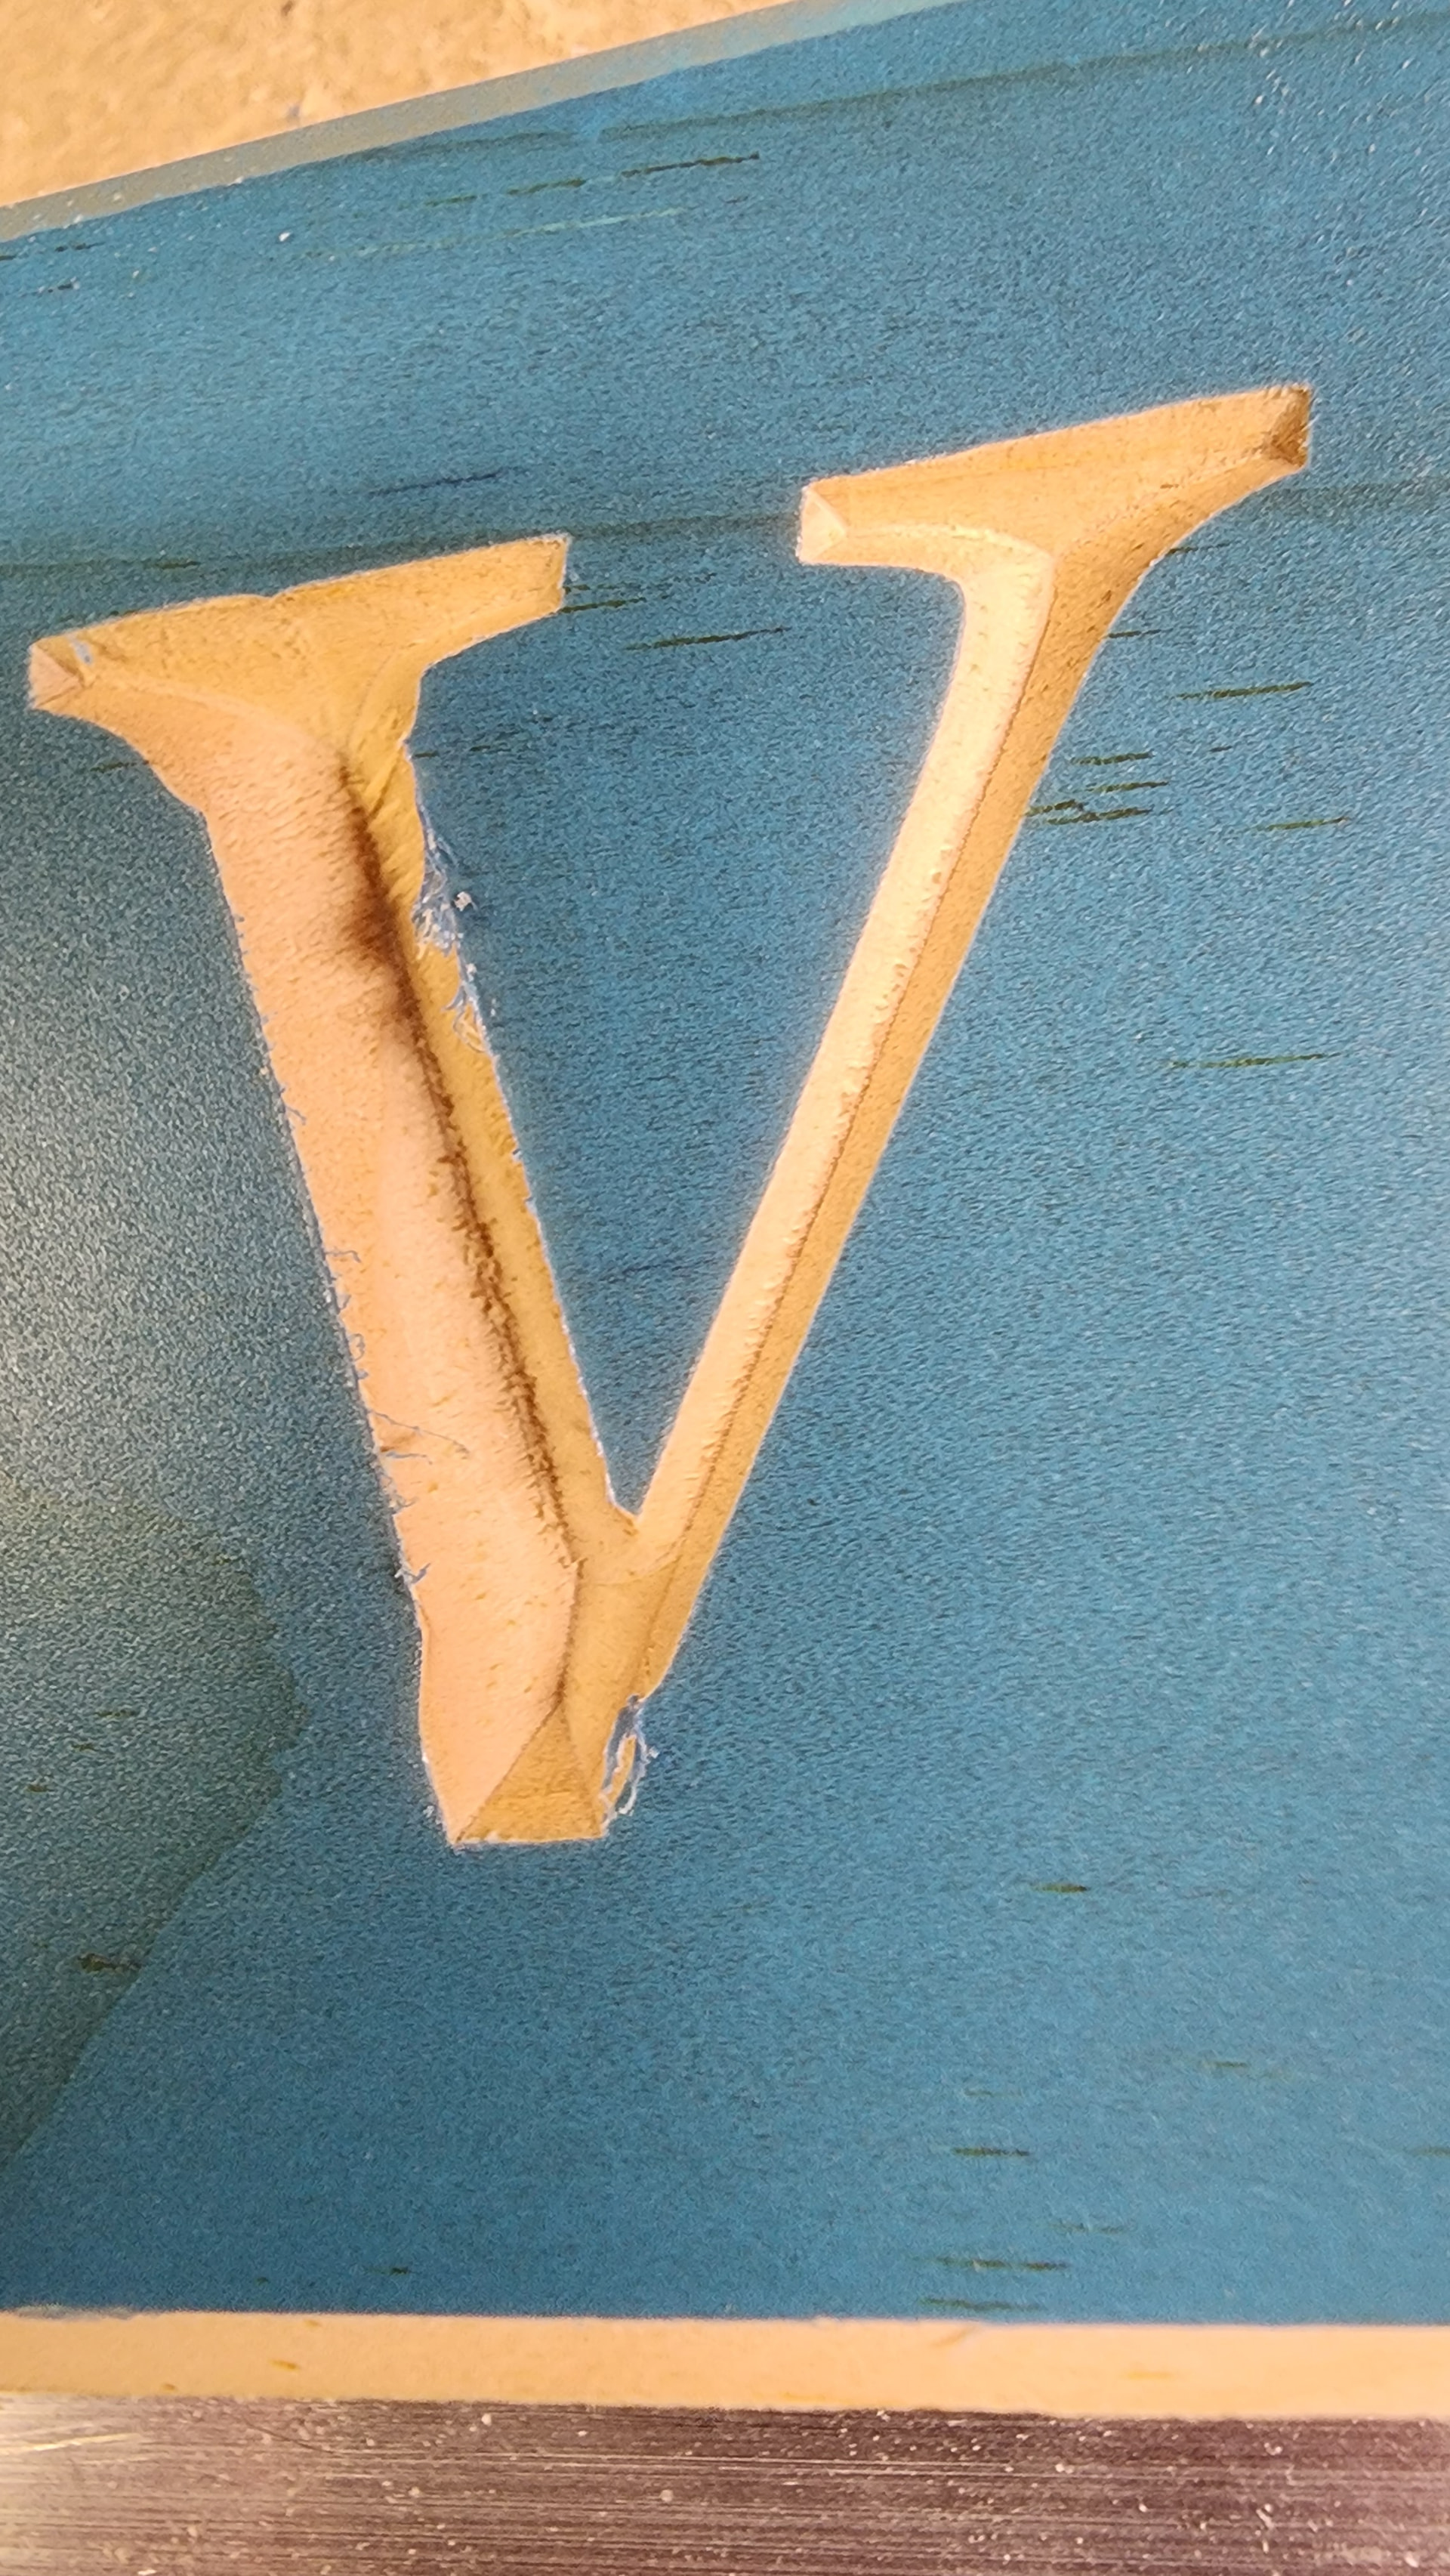
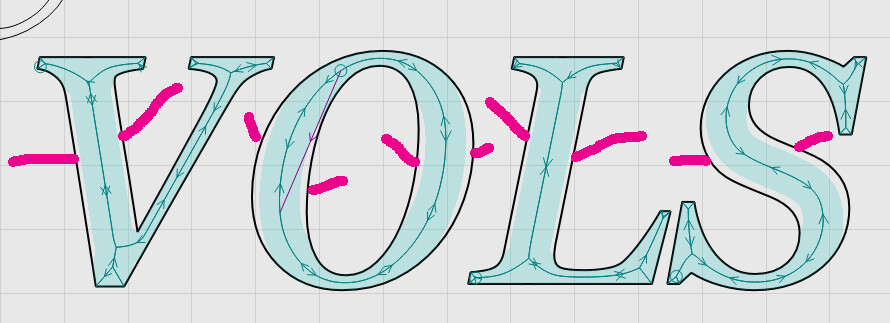This problem may be related to the way the V-Carve works. When doing small letters I’m getting a smooth cut but when the letters get bigger then I’m having some raggedness along specific areas. Please see pictures:
Could you go into a little more detail about what cutter you’re using, specifically - Up/down cut, or square?
From the paths it looks like you’re getting a full-depth carve, which means one side of the cutter is climb milling and the other side is conventional.
You have me at a disadvantage. I have never used this product. A quick video suggests sealing the surface before appling the mask. Is it possible the mask is wadding up under the cutter and causing that effect?
I also get the impression the mask is used for relief carving, but your letters look raised. Is this an optical delusion?
How are you applying the Oramask? When I put it down, and I use a lot of it, I first press it down with a silicone blade and then follow up with a 4" rubber roller. I press down very hard on the rubber roller.
I’ve experienced what you are getting but typically only on recarves where I applied a 2nd layer of Oramask 813 over previously carved lettering. It is a somewhat different tear out though.
I think your problem may be related to a rough grain surface where there are small air gaps under the Oramask. Try the roller trick and see if that improves the situation.
The wood is grainy yes. I resurfaced and fine sanded prior to coating the wood with a clear coat. I believe the problem only occurs at the full depth cutting.
This is picture of resurface wood that is sanded only, I has a better response,
Note that the wide side of the letter has hairy edges while the narrower right side has a clean cut. At the bottom right is a place where there is a swivel of the cut but it is at full depth.
Maybe the bit is not as sharp as it should be at the upper/widest parts of the edges? Or perhaps at the deepest part of the cut you are reaching the very high end of the carbide slip? Or maybe even just past it?
Any time I’ve ever had any tear out using the Oramask its due to bad adhesion.
You could try a thicker grade of mask. Or you could try applying it to a finished surface.
The manufacturer recommends using a rubber roller and applying to a finished surface whenever possible.
If you’re applying the mask to raw wood it could be just simply not sticking well enough. Make sure the surface is as clean as possible before applying your mask. And use a J roller to stick it down as well as possible.
The next step is using a high quality V bit. If you have carbide insert bit that would likely cut through the mask much more smoothly.