where in millmage do i find Absolute Cord
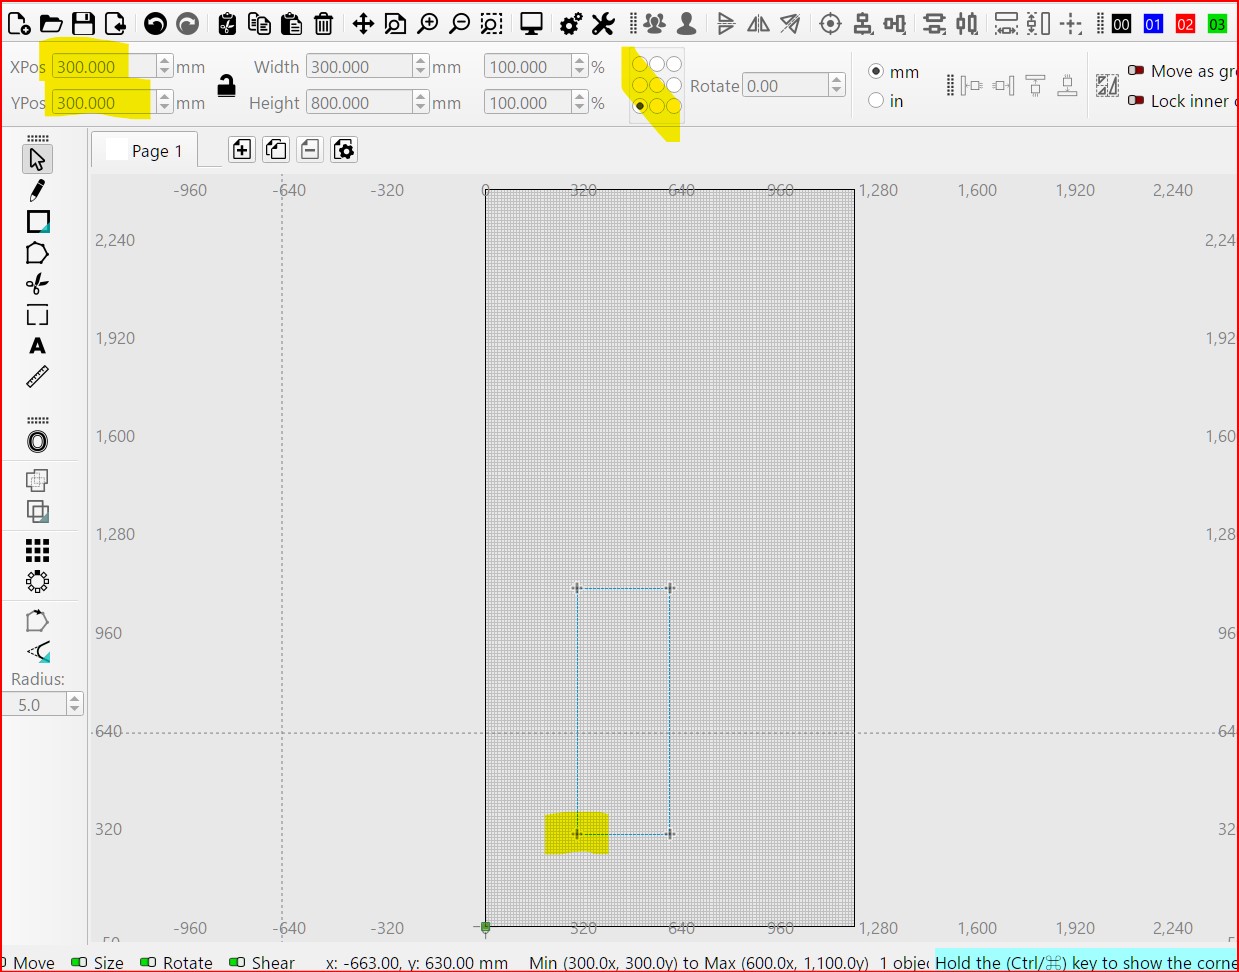
User origin
where in millmage do i find Absolute Cord
User origin
MillMage only works in Absolute Coordinates. User Origin and Current Position do not exist like they do in Lightburn.
May we ask why you need to have the User Origin feature?
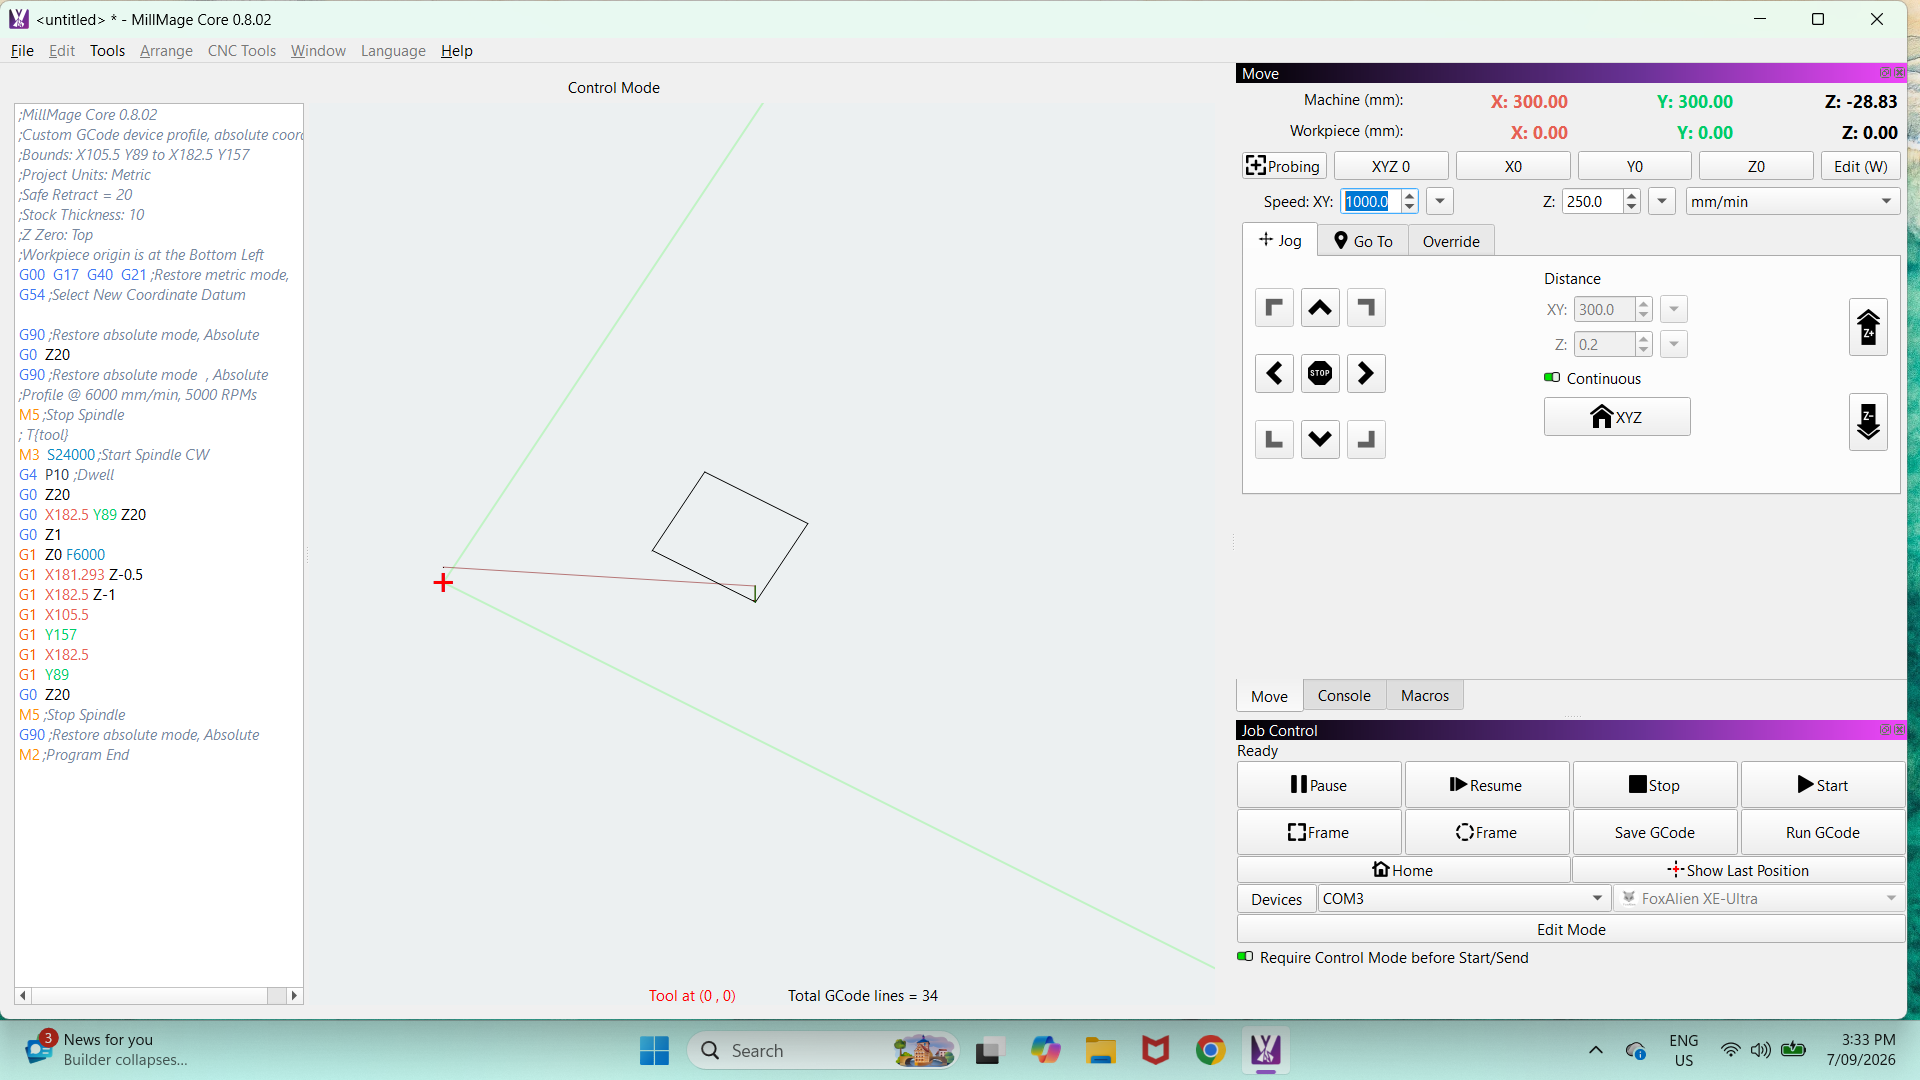
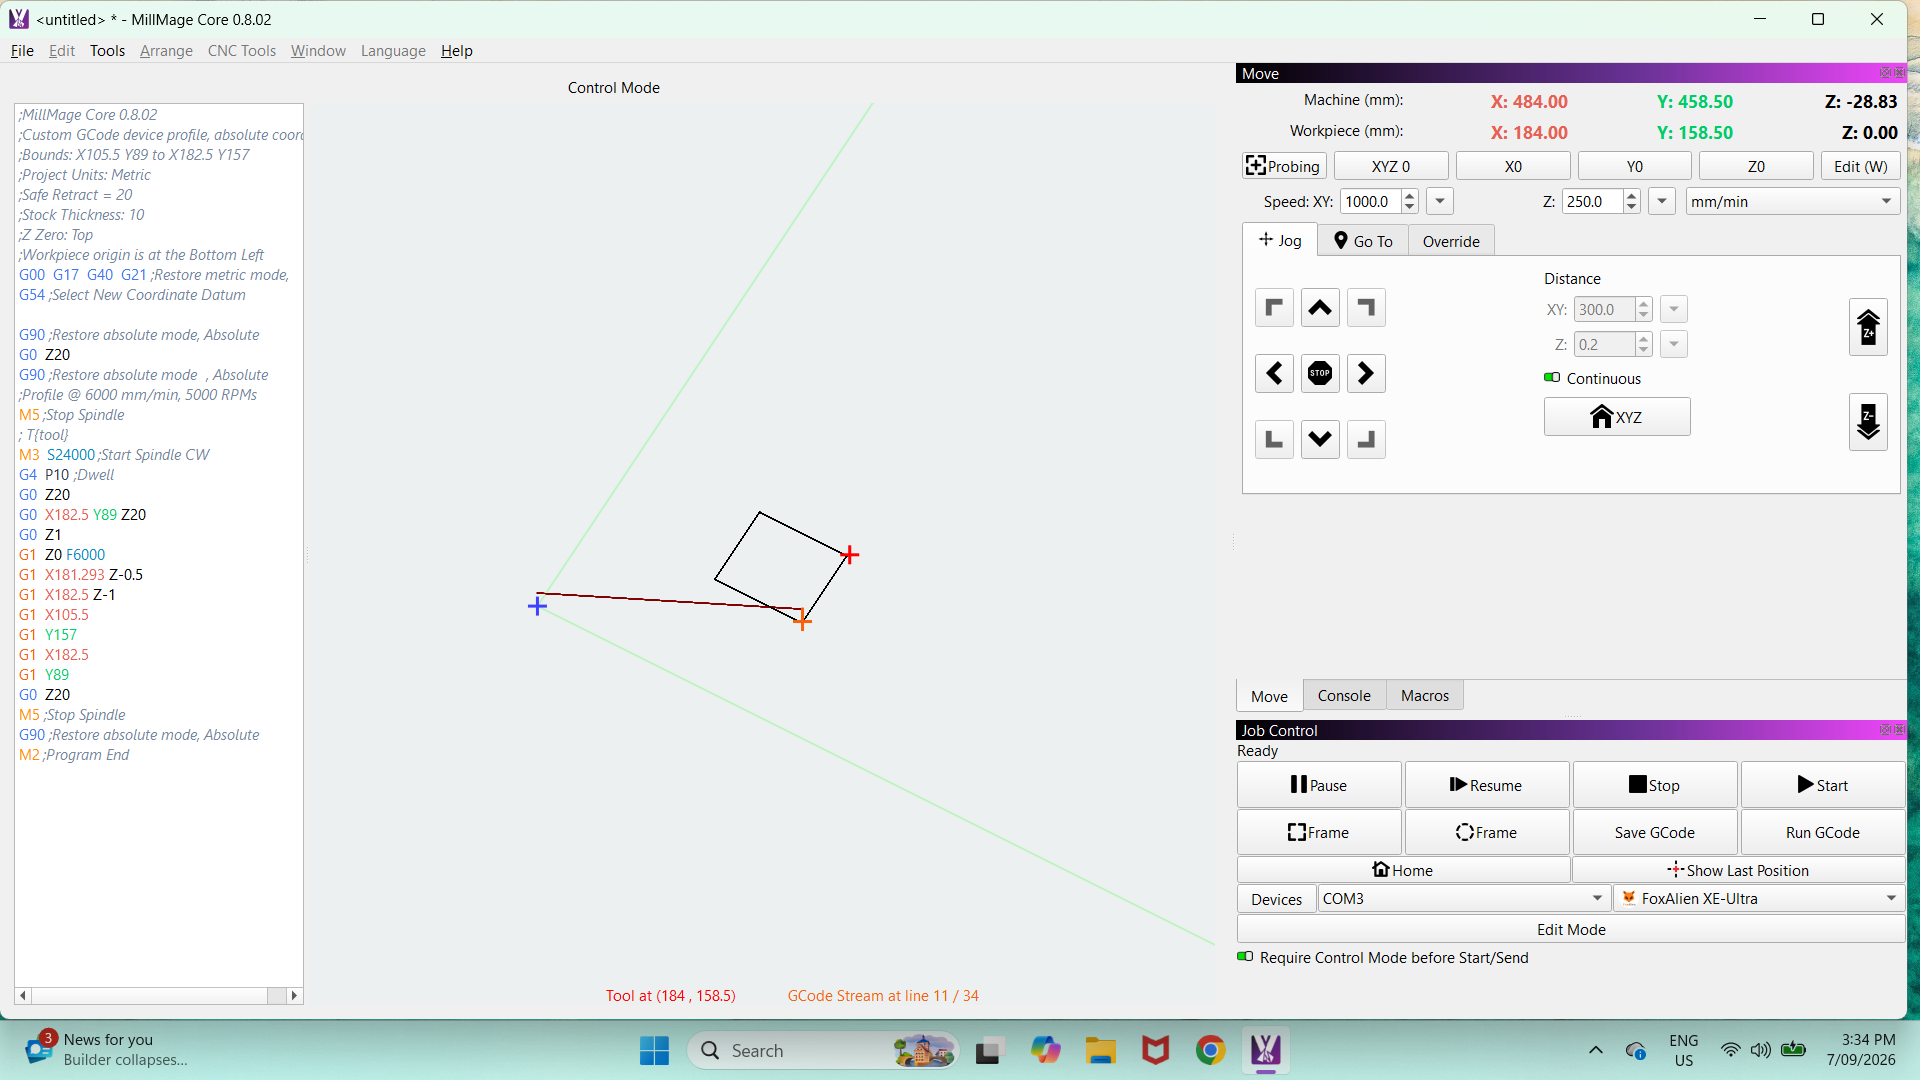
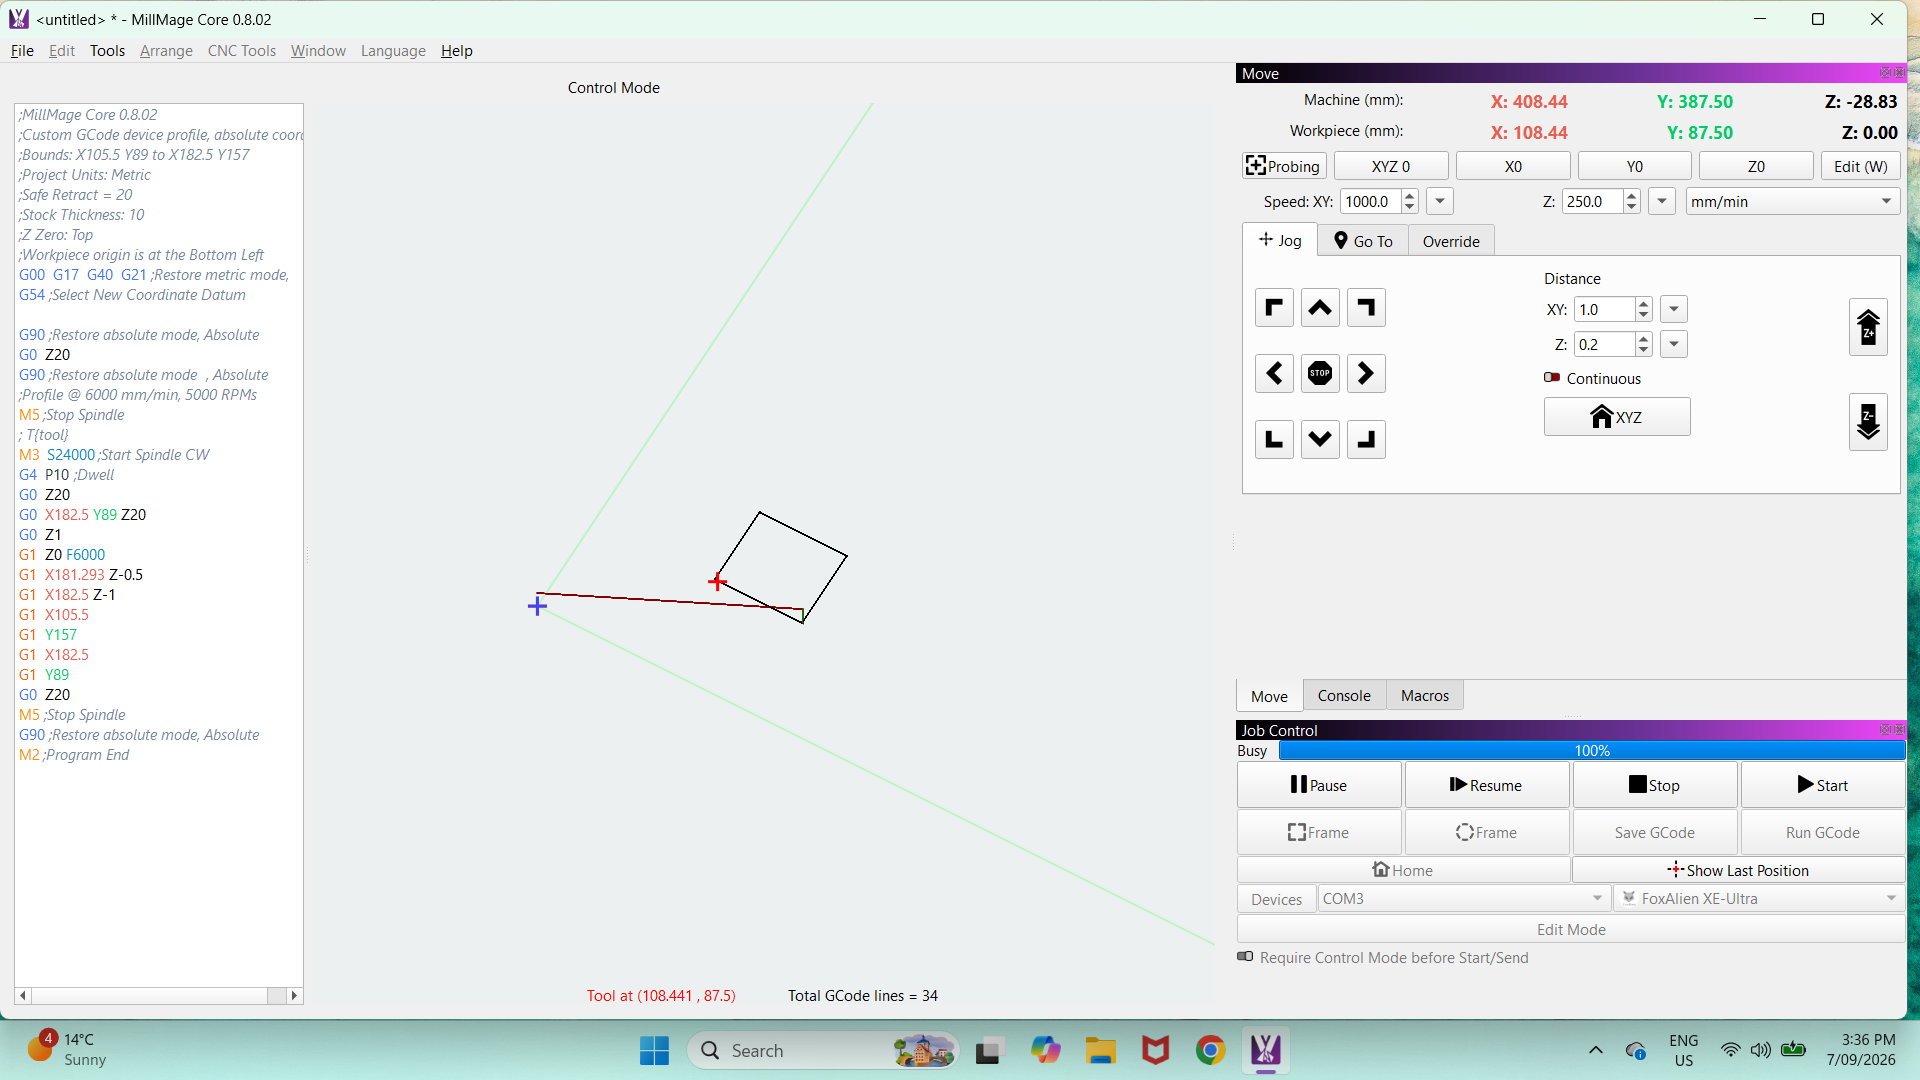
when i start a job after zeroing X Y Z the spindle want to go to where the job is on the workpiece that I have on the screen not the cordinance
it seems to flip my job over to the right than to the rear
Are you saying it engraves backwards, or is it not starting where you think it should?
what cordiancess are you talking about ?
going to where job is on workpiece on screen is normal
are you new to cnc ? are you treating it like a laser
if so i think you may be misinterpreting how workpiece works
can you put a screen shot and ur mage file up so we can look
is this the scenario of whats happening say your bed is 600x 600 , you create a work piece of 300x 300 ,design is in center of that workpiece you drop the board on your bed say in centre, but when you start job spindle dosent go to where board is ?
the reason being is MM works off your project size not your bed size
there is a way to achieve this with a template
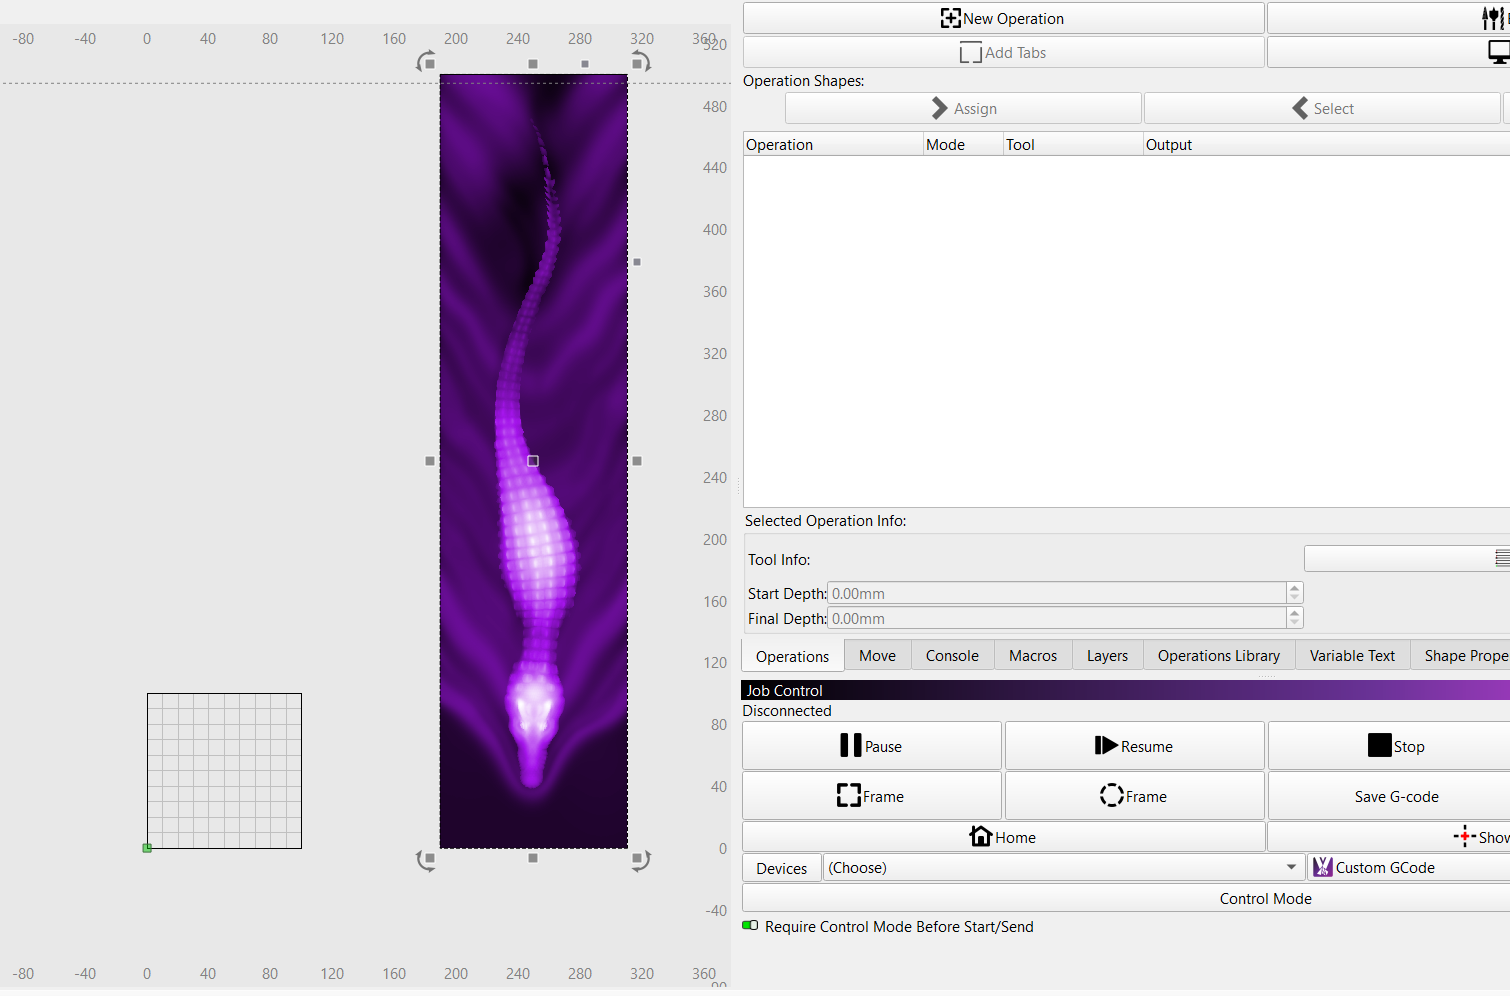
this is template i use it is full size of my bed. 2400 x 1200 the blue square is marked out on my table and shape is lock on the template , when im doing small pieces i drop them there and probe from bed
what machine do you have
Without the .mage file, we have to make some assumptions based on the postings in this thread.
[1] You did not show us where it actually goes in relation to your machine table, so I cannot improve on the math calculations.
[2] You did not provide the .mage file, so we cannot use your actual settings for testing.
[3] Is it possible leaving the Origin alone and using Absolute Coordinates will simplify the setup and operation of your projects?
[4] If you want to do it your way, then you must have a good grasp of coordinate systems, graphic quadrants, and machine geometry.
[5] If I said anything you feel is insulting, that is not my intention and I apologize. But I did say assumptions would be made based on what has been provided so far.
Hi, my fault, all OK, I was used to using lightburn and setting the start of the job with the laser head.
the only problem I have is the spindle speed. I set it in the tool selection but when i start the job it goes to the full 24000rpm. The only way I can slow it down is in the override section when the job starts.
I have a VFD 1.5kw spindle.
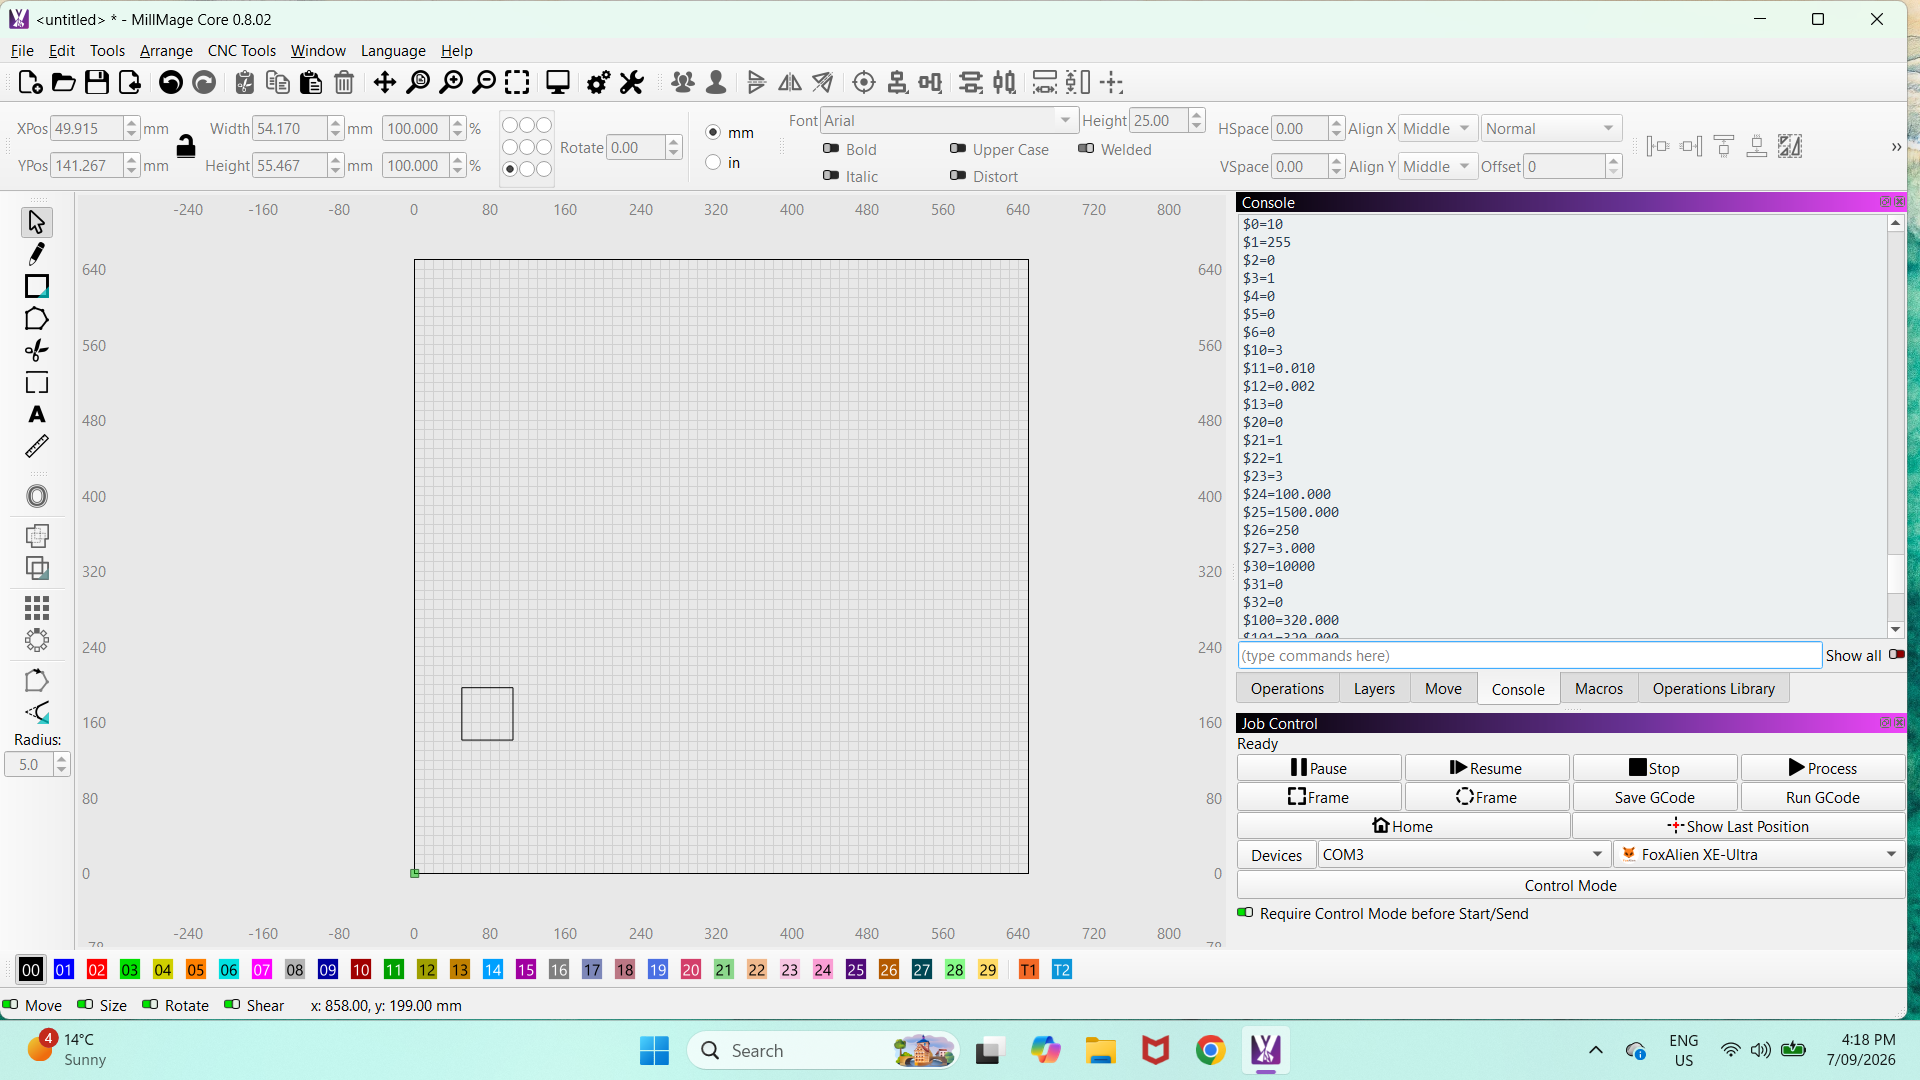
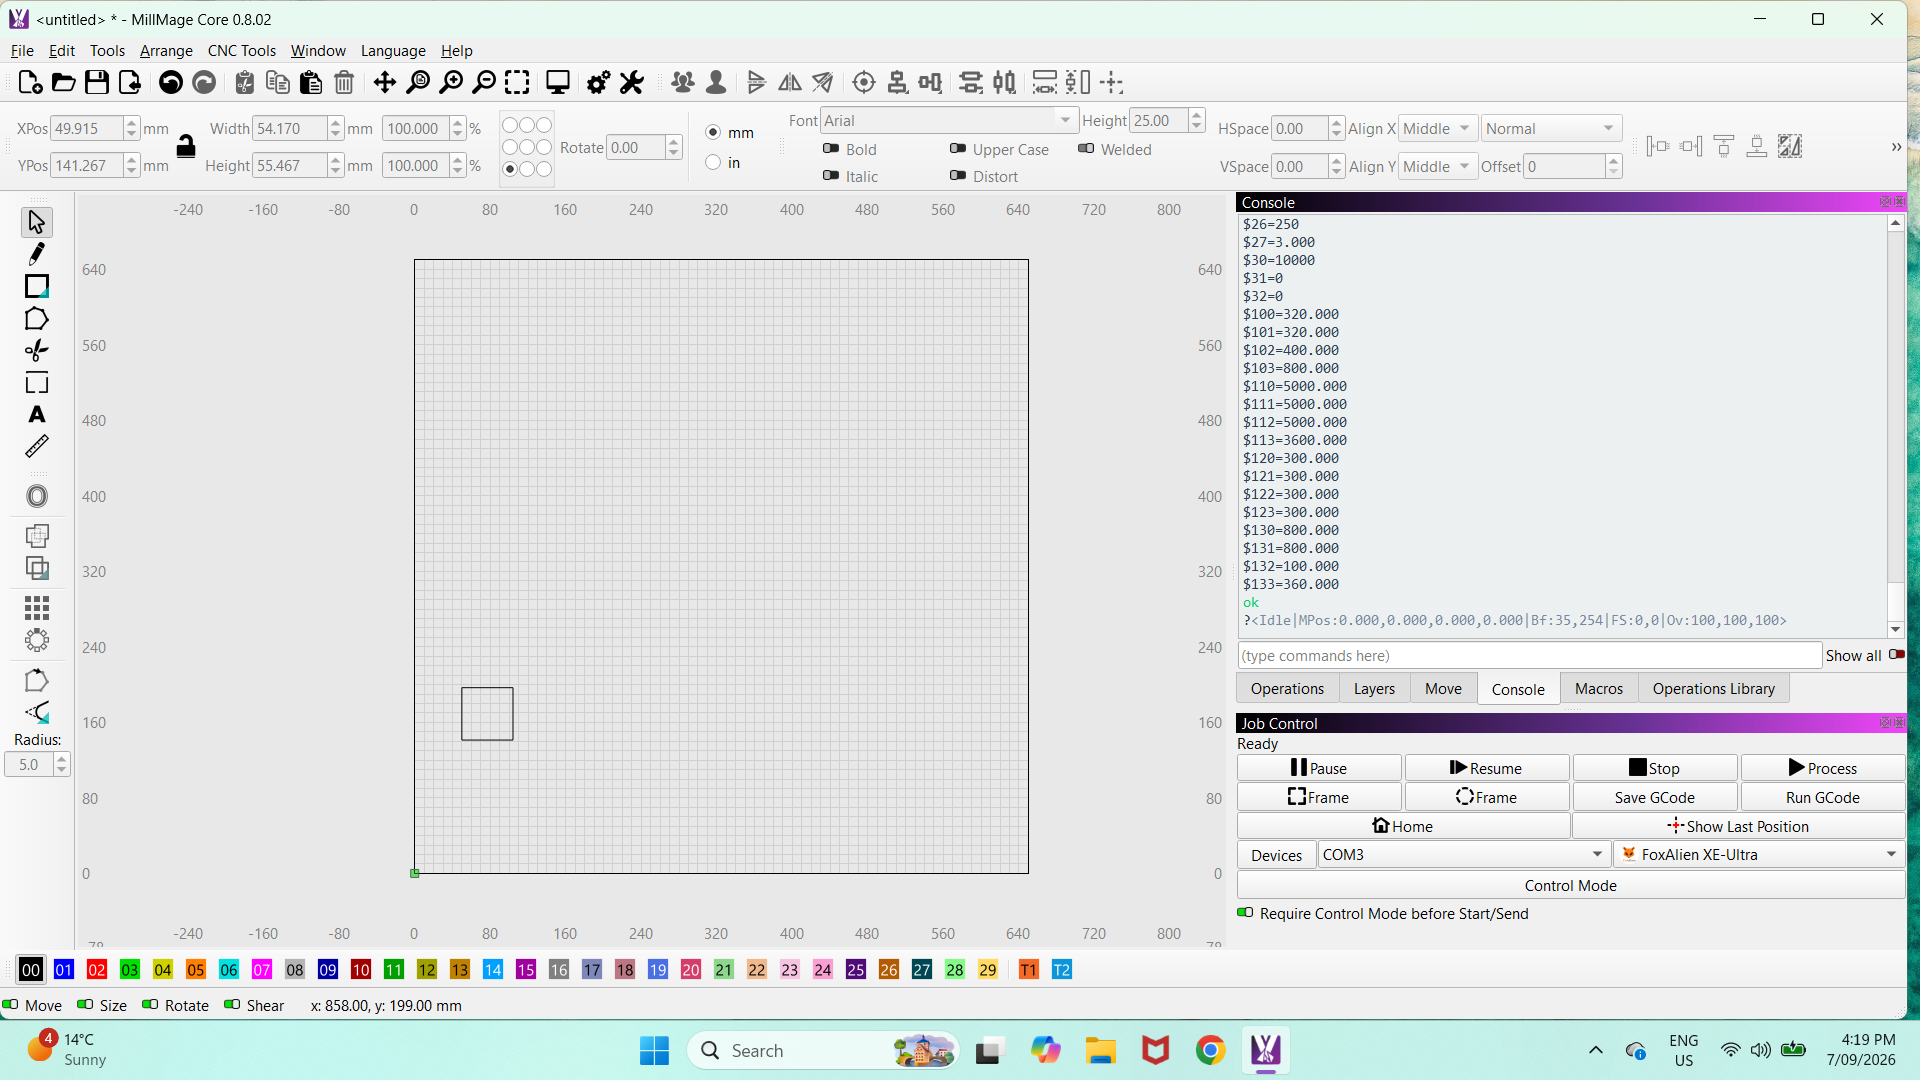
$30=24000
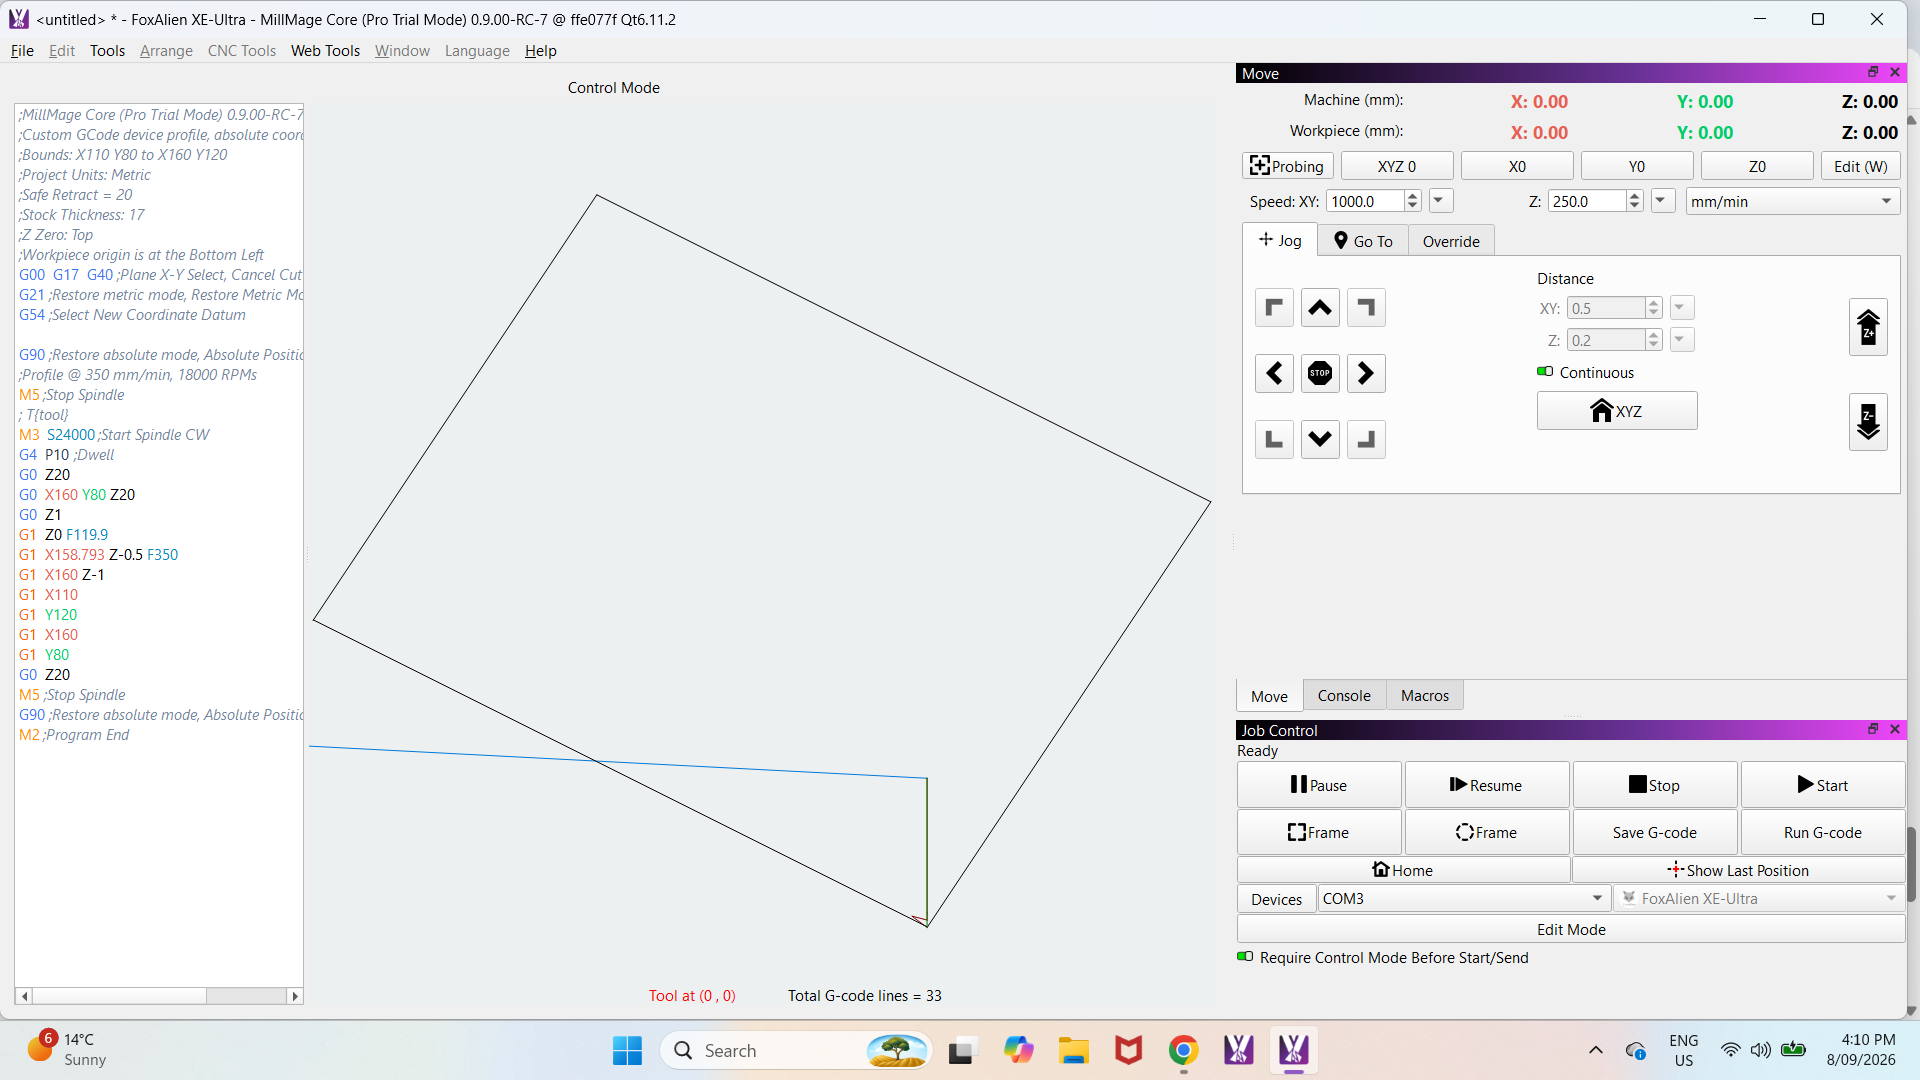
G Code tool on M3 S24000 G4 P10
When I hit Process I don’t get the speed and feed down the bottom.
Yeah, that is both a blessing and a curse. 
@wanderingtruckie asked what machine did you have, but you did not answer. Some mills have VFD drives that are not managed by the controller, so MillMage cannot manage it either. But…
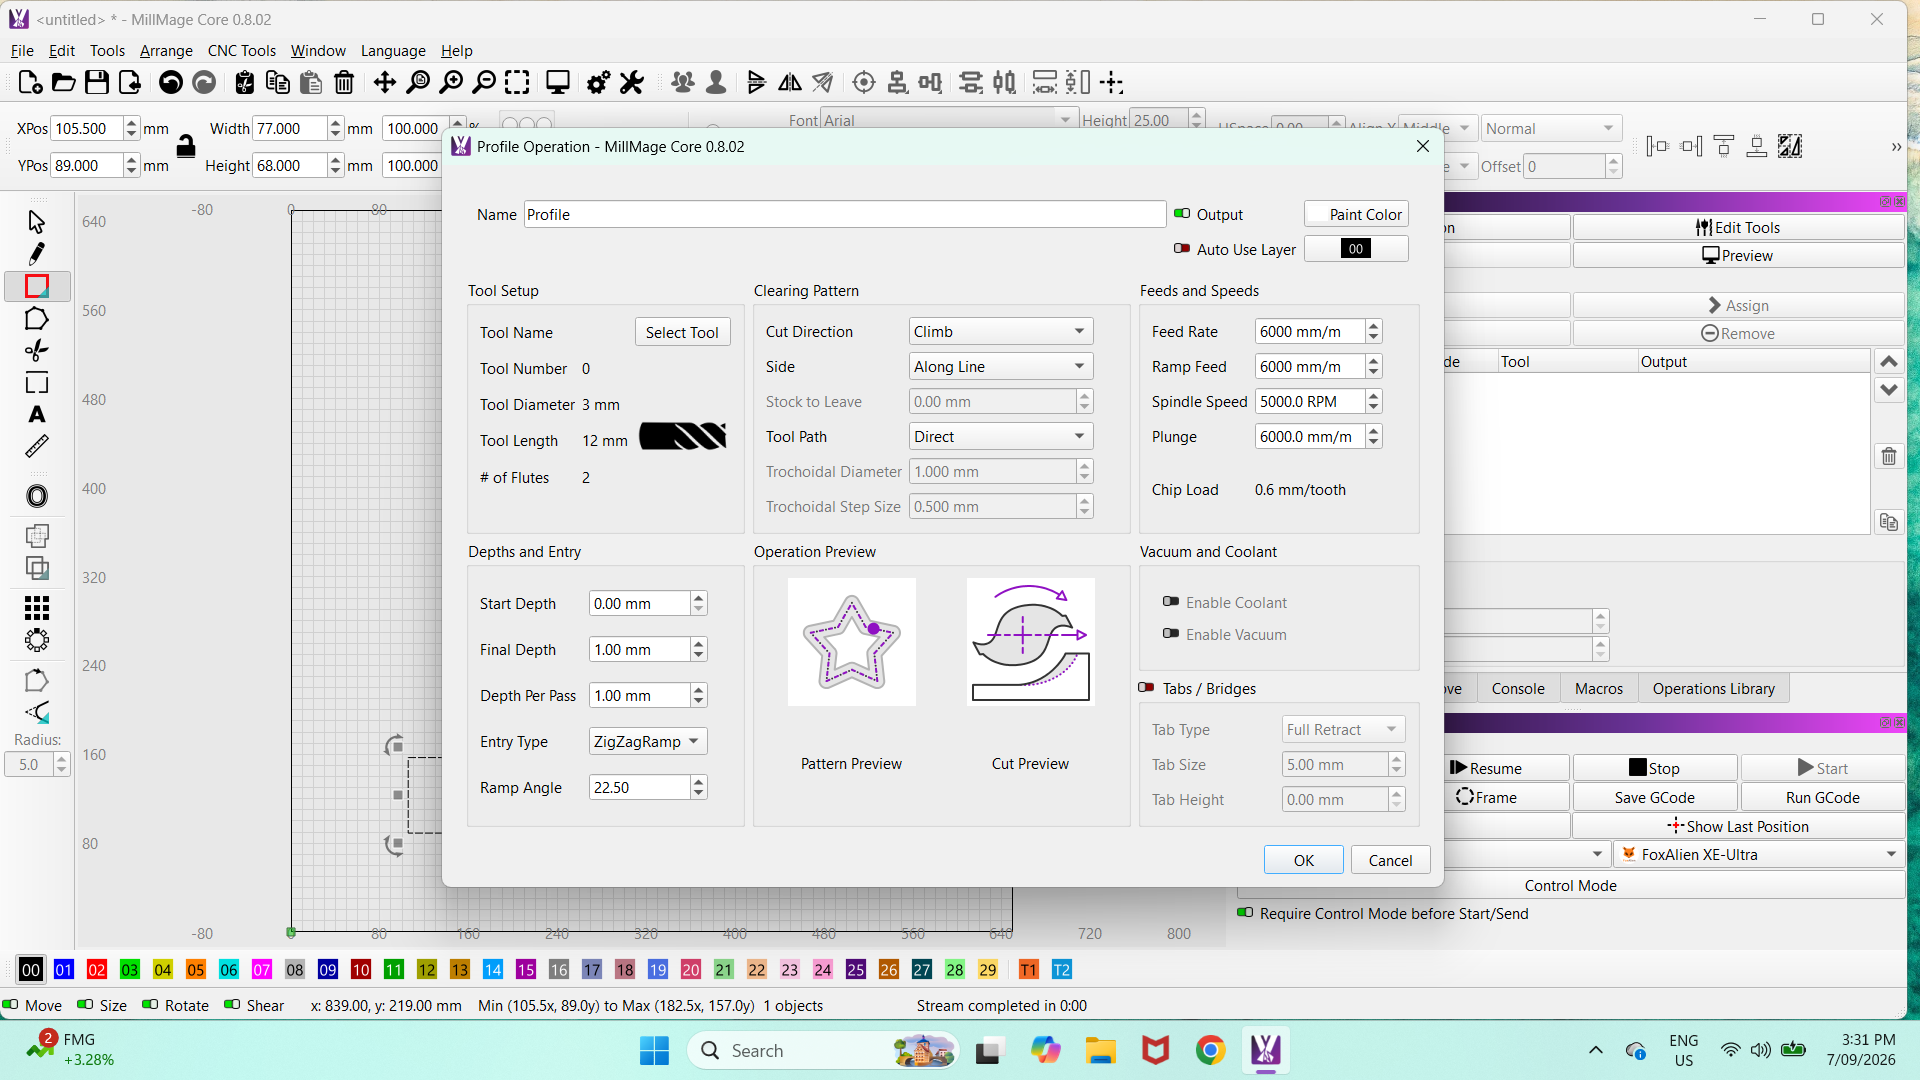
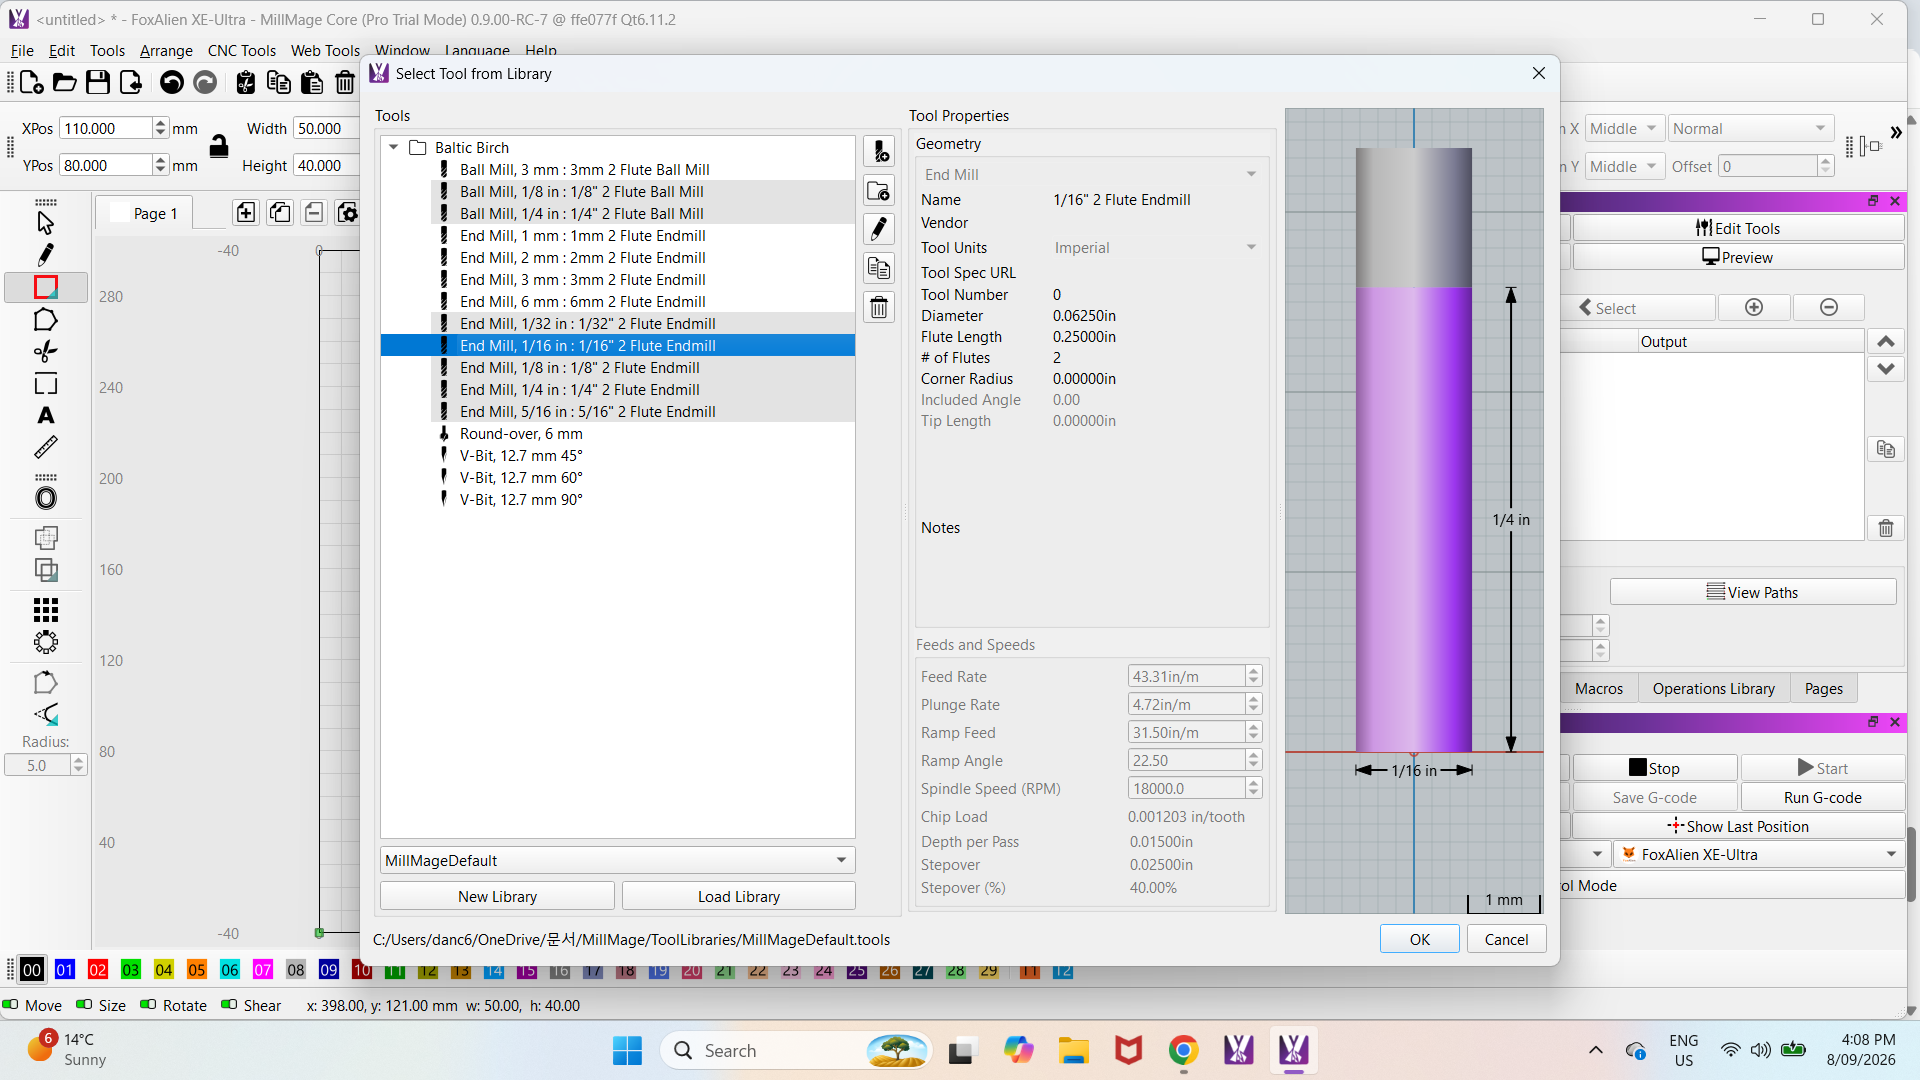
This indicates that MillMage CAN control it. Now the question is, “Where are you setting the spindle speed?” If you set it as 24kRPM in the tool definition area, that is what it will run. And you can override it in the Move window while running, as you discovered.
If you want to use the same tool on different materials, where different speeds are required, then you can define it as another tool with different speed settings, or chip loads. You can even define all your tools into a new category in the Tool Library. It is quite flexible when setting up.
You likely know all of this, but we will get a lot of new users reading these MillMage posts and might benefit. 
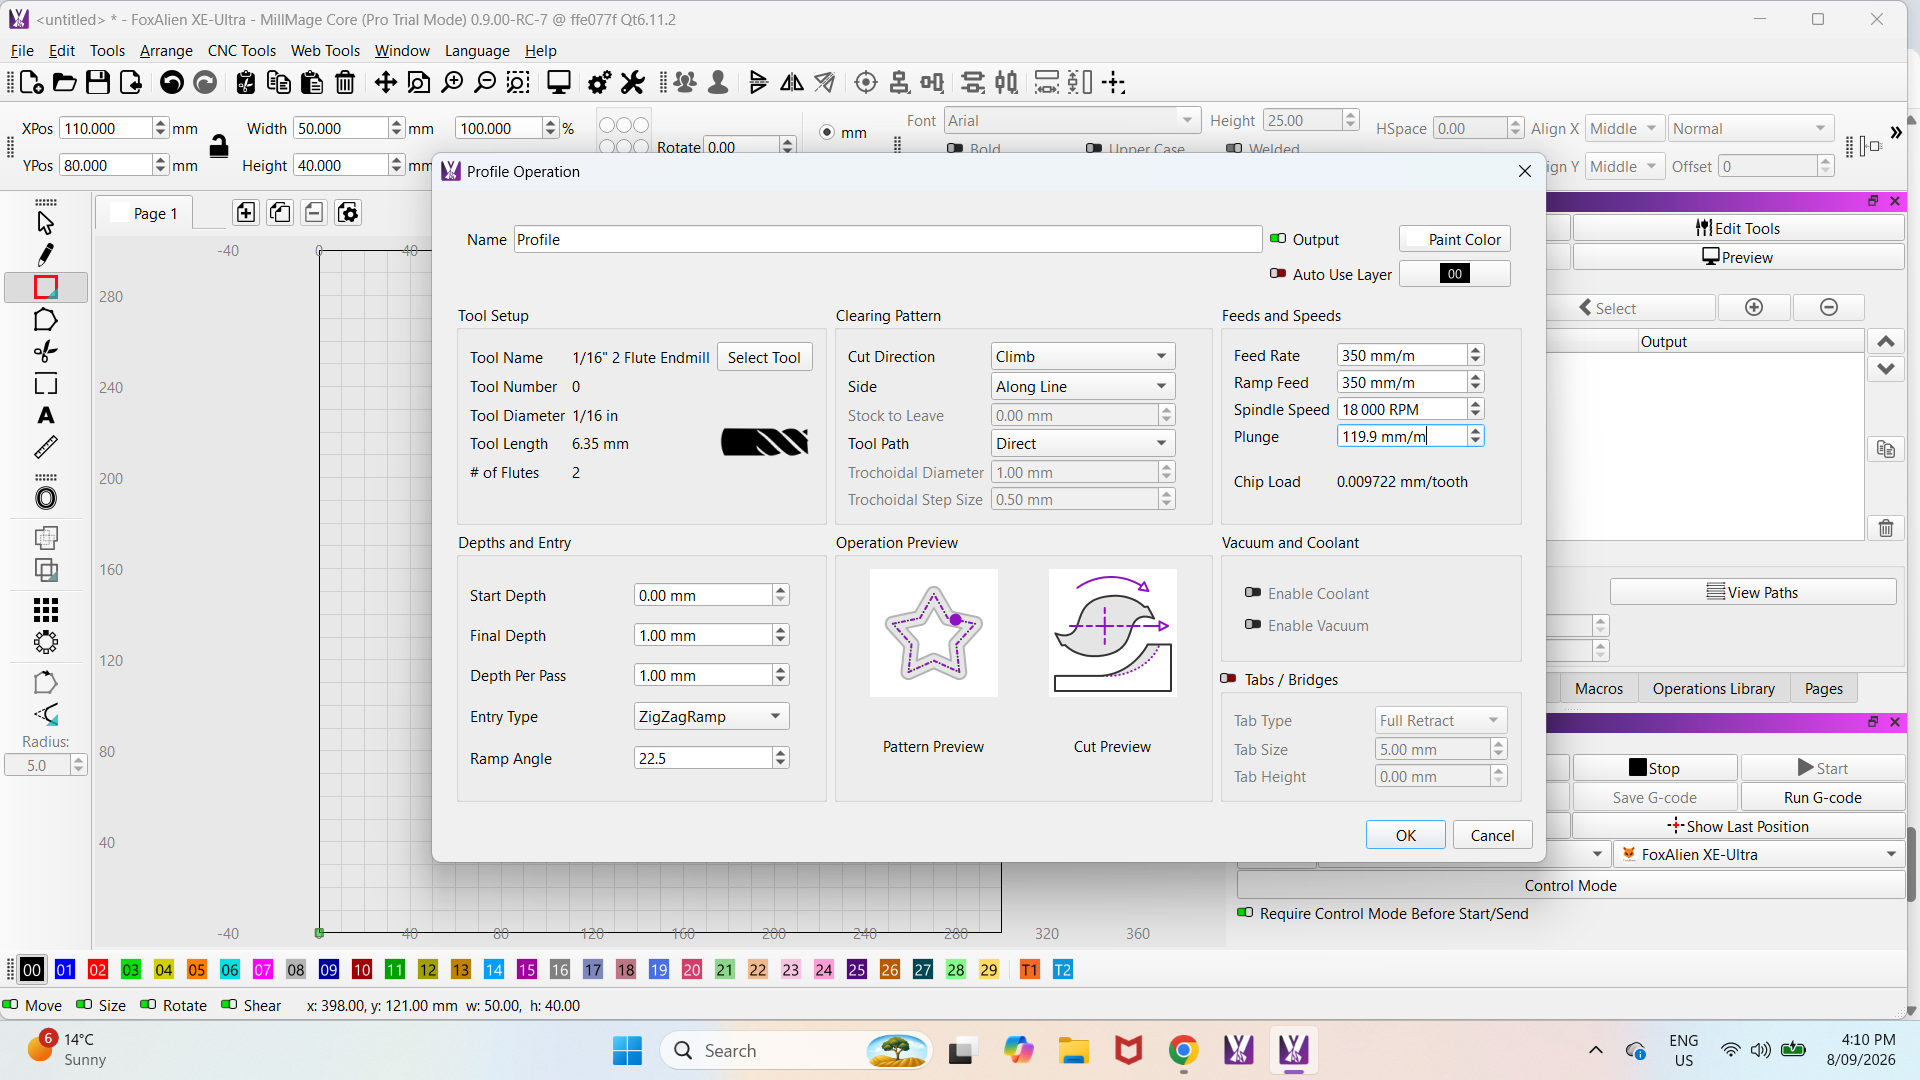
It appears you assigned 18,000 RPM to a tool, but it outputs 24,000 RPM. That is a different issue that requires you upload the .mage file so it can be investigated. What I do not see in the GCode is a tool selection (tool number).
MillMage
AutoSave_4024.lbrn2 (66.6 KB)
AutoSave_5630.lbrn2 (22.6 KB)
I hope this is the file that you require.
I am setting the spindle speed in Profile Operation.
I have a Foxalien VDF 1.5kw PWM controller.
MillMage design files have the .mage extension, not .lbrn2 like you supplied.
That is the only .mage file I can find.
I opened millmage, opened File than hit open. there are two lightburn files and that one, is there somewhere else I can find the .MAGE files. I tried to do a copy and past but that was too big of a file so I copied the link.
You decide where you save your project files. Do a Windows search for “.mage” or “.lbrn2” to find them. Let us know how it goes…
Spindle Speed Test.mage (11.8 KB)
hope this one can help.
Spindle speed set at 1800 but goes to 24000rpm
Pretty sure you meant 18000. How are you telling the difference between 18000 and 24000?
What is the value in your $31 parameter? It should be Zero. If this is not the issue, then…
Set your $30 on the controller to 5000, your tool RPM’s to 500, and report what effect that has.