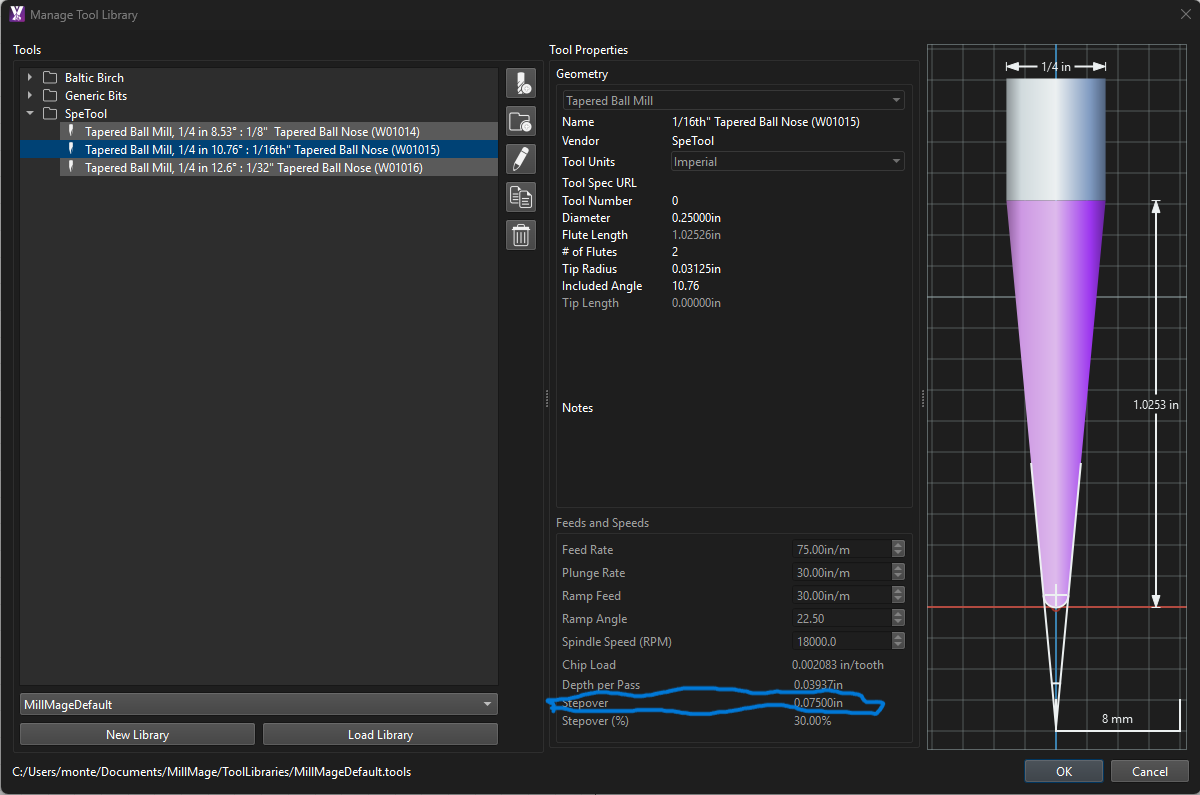
In the tool properties, should this step over be calculated on the diameter of the shank of the bit or the diameter of the tip of the tapered bit? It seems like the software is using the diameter of the shank for these calculations. Is this correct
Not sure, but I have seen recommended stepovers of 5%-8% (0.0125" - 0.020" for your tool) for Ball End mills doing contouring work. I think 30% stepover is a bit too much for this tool. The 2 numbers I stated are well within the tip radius (0.03125") of your tool.
Not a pro, but it makes sense you should not exceed the radius of the tool for contouring work.
I can’t help with Millmage but in Aspire, the % stepover on tapered bits is related to the tip diameter (2X tip radius) and for end mills with no taper tip and bit are same diameter. So from your example with a tip radius of 0.03125 and stepover of 30% I would get 0.01875 on my software.
Ball end and flat-tip taper mills are the only bits that would be able to work this way, and doing so causes other problems - There are numerous fields in the software that work on “percentage of bit radius”. We initially tried making it work the way you suggest, but it got confusing, and broke a bunch of things.