The first question: is it really acrylic? If it’s not from a reputable source, the “acrylic” may be ABS (or something similar) intended for rotary-tool cutting that won’t cut with a laser no matter how much you cuss.
For engraving, good reuslts from a 100 W machine will require more speed and less power than your tests show. My 60 W tube fires reliably at 10% and yours is on the edge, so run a Material Test from 10% to 20% with speeds from 200 mm/s to 500 mm/s (or faster, if it can outrun mine).
I use these settings for Trolase light engrave:
- 400 mm/s
- 15% → 10-ish W
- Bidirectional
- 0.1 mm Line Interval
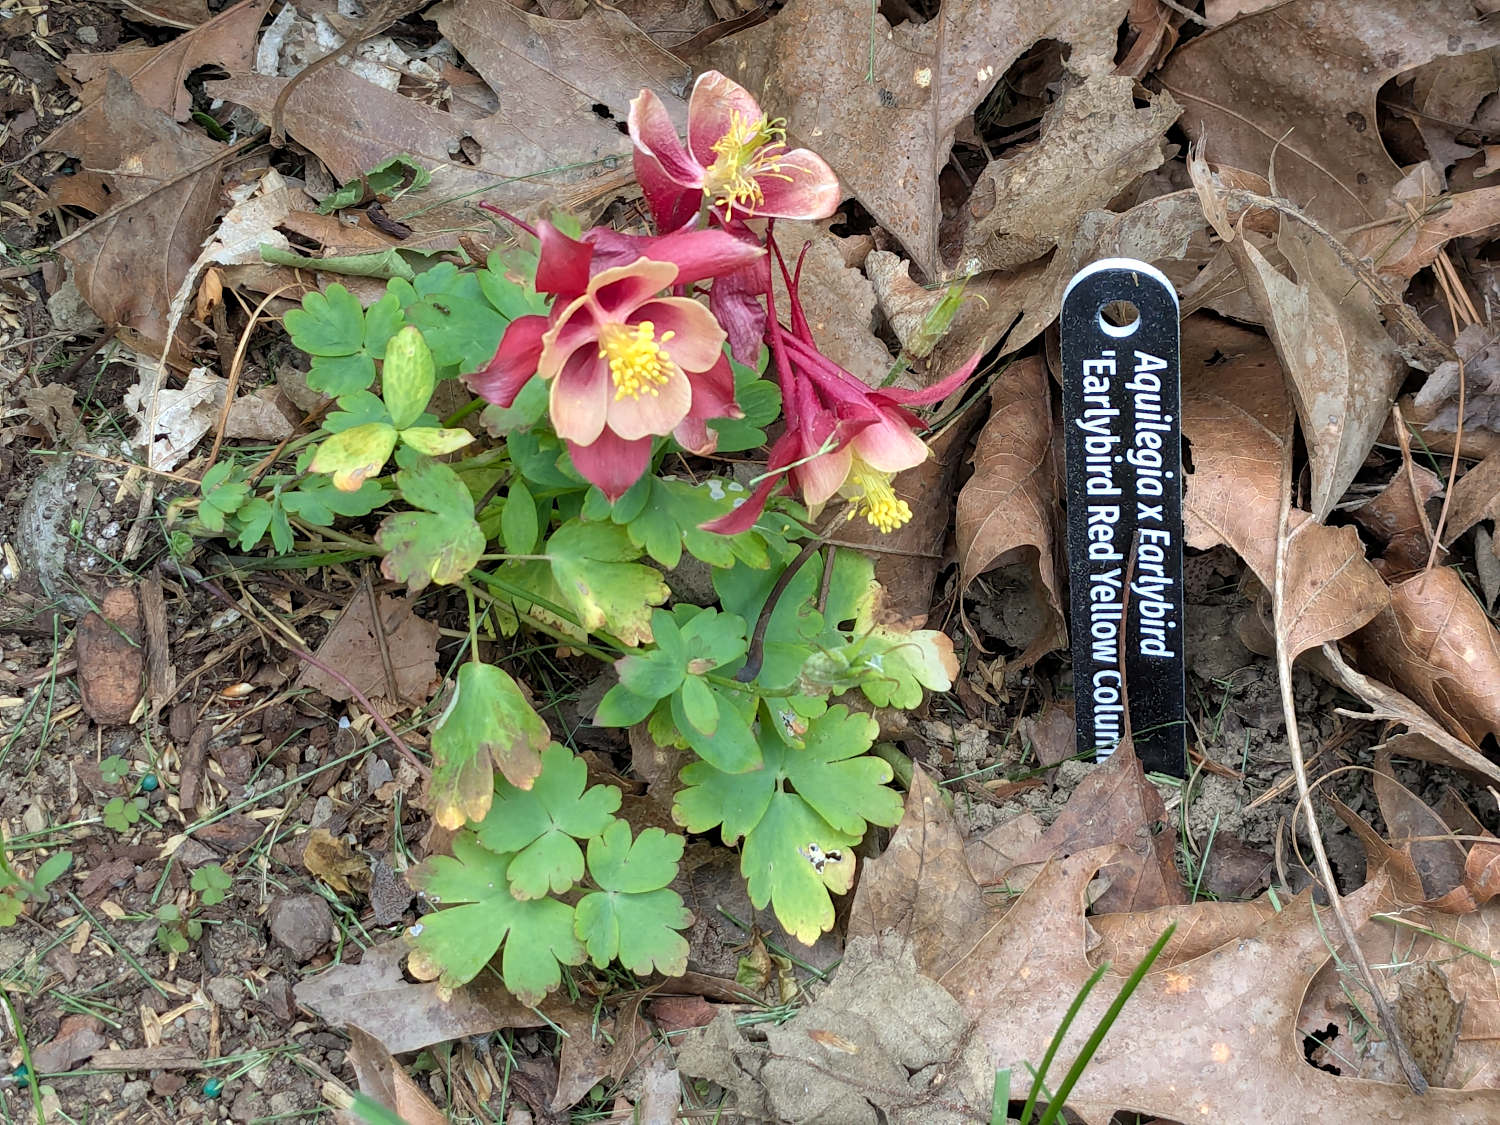
Which produced nice results on plant tags:
For cutting 3 mm Trolase:
3 mm Trolase cut
- 15 mm/s
- 60% → 35-ish W
The terrible cuts in your test suggest the beam shape isn’t quite right. Verify the focus by running a ramp test, then a Material Test around the power & speed I use.
If the cut remains terrible, the tube may not be resonating in TEM00 mode. This discussion covers what that means, what to do, and what to look for:
Let us know what you find as you go along!